

What are the main structural parts of an Autonomous Mobile Robot (AMR), and how are they built? The most common AMR structural parts are the chassis, frame, caster mounts, sensor brackets, and battery housing. Manufacturers use CNC machining, injection molding, sheet metal fabrication, and additive manufacturing technologies like polymer 3D printing. Unlike AGVs, AMRs move around in flexible ways, so every part must be lightweight but strong. Composite molding, which uses open or closed molds, is becoming more popular for high-strength components. This guide gives practical tips for picking a process based on volume, cost, and strength.
Common AMR Structural Parts and Their Functions
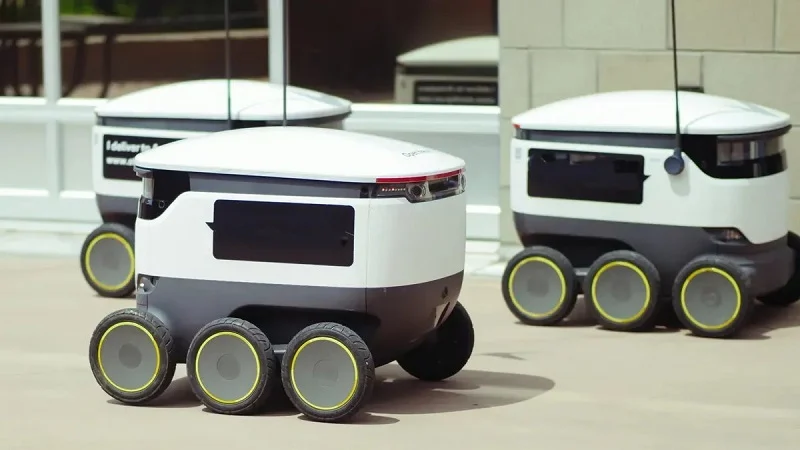
Every AMR depends on a group of main structural parts that work as a team. Each part has a certain job to keep the robot steady, accurate, and safe from its surroundings. Knowing these jobs helps engineers make good choices about design and production.
Chassis and Frame: Load Support and Rigidity
The chassis is the main support of any AMR. It holds the full payload and keeps every other part in place. A well-built chassis fights twisting and bending during speeding up, stopping, and turning. This stiffness keeps sensors lined up and stops navigation mistakes.
Design for Payload, Damping, and Alignment
Payload capacity shapes chassis design from the beginning. A robot carrying heavy inventory needs thicker walls and stronger joints than a light unit. Damping also counts. Shaking from motors and wheels can blur sensor readings. Engineers add rubber isolators or tuned mounts to soak up shock. Alignment matters just as much. If the frame twists even a little, a laser scanner may aim off-target. That misalignment creates safety risks and lowers inventory visibility.
Integration of mounting points for motors, batteries, and sensors
Mounting points must be exact and repeatable. Motor mounts need tight tolerances so drive wheels stay parallel. Battery mounts must hold weight and allow quick swaps. Sensor mounts require flat surfaces and exact hole patterns. A small error in hole placement can shift a camera’s field of view. This integration calls for careful engineering from the first sketch.
Structural Part Function and Integration
Past the chassis, several smaller parts keep an AMR moving and sensing reliably. Each one has its own clear job.
Caster mounts and wheel hubs for stable mobility
Caster mounts hold the robot’s weight at the front or rear. They pivot freely and let the AMR turn in tight spaces. Wheel hubs link drive motors to the wheels. Both parts must resist wear and handle repeated impact. A weak caster mount can crack after thousands of cycles. That failure stops material handling right away.
Sensor brackets and mounting plates
Sensor brackets hold lidar, cameras, and proximity sensors. They must be stiff enough to stop vibration yet light enough to avoid adding mass. Mounting plates give flat, stable surfaces for these brackets. Precision here directly affects navigation accuracy and safety. A bracket that flexes by even a fraction of a millimeter can cause costly errors.
Additive Manufacturing Potential for Complex Brackets
Complex bracket shapes often challenge traditional production methods. Additive manufacturing technologies offer a way forward.
Polymer additive manufacturing
Polymer 3D printing builds brackets layer by layer. This process handles organic shapes, internal channels, and lattice structures that subtractive methods cannot easily create. Engineers use it for prototypes and low-volume production runs. The technology shines when a bracket needs custom features or weight-saving pockets.
構造健全性に関する考慮事項
Printed brackets need careful design for strength. Layer orientation affects load capacity. A bracket printed with layers perpendicular to the main stress direction may delaminate under load. Engineers must also account for material properties. Some polymers absorb moisture and lose stiffness over time. Testing and validation remain essential before deploying printed parts in demanding applications.
From a practical perspective, companies like NOBLE, a leading manufacturing company in China, bring exceptional service capabilities and professional machining expertise to this space. They help clients move efficiently from prototyping to mass production of AMR structural parts. Their experience across multiple processes ensures each part meets real-world demands.
Manufacturing AMR Structural Parts: Key Processes
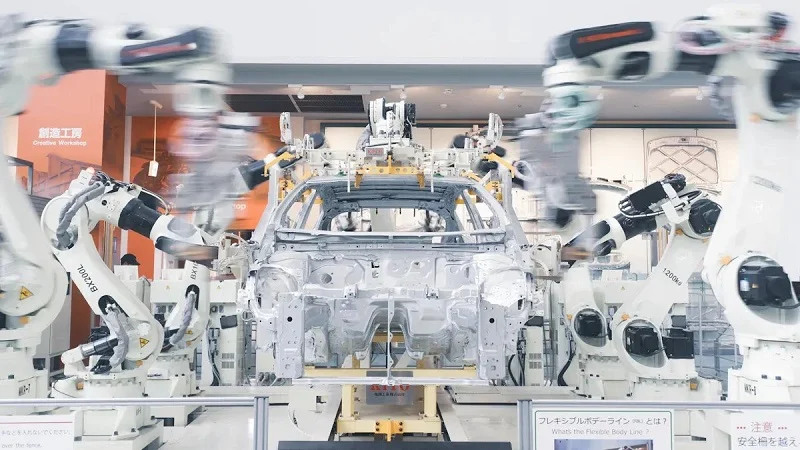
精密部品のCNC加工
Ideal for low-to-mid volume custom parts with tight tolerances
CNC machining works great for AMR structural parts when you need small or medium batches. For runs under 500 units, this manufacturing process gives you high precision without big upfront tooling costs. The first part and the hundredth part cost about the same. That steady pricing helps when you test new designs or build a pilot fleet. For a steel bracket weighing about 1 kg, a batch of 50 parts costs $100 to $300 each. At 1,000 units, that price falls to $50 to $100 per part. The main advantage here is accuracy. CNC can hold positions within ±0.025 mm. That level of precision keeps sensor mounts and motor brackets lined up. When a robot needs exact sensor placement for safe navigation, that accuracy is important. These engineering components depend on digital programming and standard cutting tools. You do not need expensive molds. That makes CNC perfect for custom work where shapes change often. The process works well for low-to-mid volume production.
Aluminum, steel, and plastic materials
Aluminum 6061 is the top choice for most CNC-machined parts. It gives you a great mix of strength and weight. Setup times are short. Cycle times are fast. Tool wear stays low. For general-purpose brackets and chassis components, aluminum gives the best performance for the cost. Brass works well for small batches where you need function and looks. Stainless steel and titanium are harder to machine. They need longer setup, slower cutting, and more costly tools. That raises costs for low-volume runs. Plastics like ABS and nylon also work on CNC machines. They are lighter and cheaper, but they are not stiff enough for many structural applications. Material waste is high with CNC. About 60% to 80% of the stock ends up as chips. That matters when you use costly alloys. But for complex shapes at low-to-mid volume, CNC machining is still hard to beat for precision applications.
ポリマーおよび複合材料の付加製造
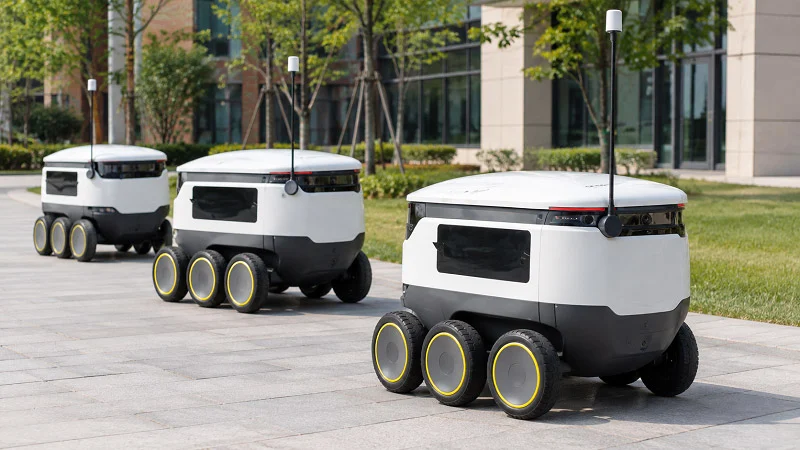
FDM and SLS for brackets, housings, and prototypes
Additive manufacturing technologies bring real flexibility to part production. FDM and SLS are the two main ways to make polymer parts. FDM uses filament that melts and builds layers. ABS parts from FDM show good impact strength — around 40.0 kJ/m² notched IZOD. SLS uses nylon powder and a laser. SLS parts from PA12 have a notched IZOD impact strength of about 34 kJ/m². Both offer flexural strength around 56 to 58 MPa and a flexural modulus near 1.8 GPa. Nylon stands out for its toughness and heat resistance. It handles fuels, oils, and grease well. That makes it great for parts that take abuse. The real benefit of 3D printing technologies is zero tooling cost. There are no molds or dies to buy. Lead time is hours or days instead of weeks. That makes these methods perfect for prototypes and runs of 1 to 500 units. You can build complex geometries with internal channels and lattice structures. No other process can match that geometric freedom. But unit costs stay flat and relatively high. For larger volumes, other manufacturing technologies become cheaper.
Cost Comparison at Different Volumes
| プロセス | 部品の説明 | Cost per Part at Low Volume | Cost per Part at High Volume |
| CNC加工 | 1 kg steel bracket | $100–$300 (batch of 50) | $50–$100 (at 1,000 units) |
| 射出成形 | 0.1 kg plastic part | $20–$50 (at 100 units) | $0.50–$2 (at 10,000 units) |
| ダイカスト | 0.5 kg metal part | $50–$100 (at 100 units) | $5–$15 (at 10,000 units) |
Open- and Closed-Mold Composite Processes
Composite molding takes additive manufacturing in a different direction. Open-mold processes lay up fiberglass or carbon fiber by hand. Closed-mold processes use matched dies and pressure. These methods create parts with excellent strength-to-weight ratios. They work well for high-performance frames and structural panels. The tooling cost is moderate. Cycle times are longer than injection molding. But for applications where every gram counts, composites deliver real value. Engineers use them when aluminum is too heavy and plastic is too weak.
Sheet Metal and Injection Molding for Volume Production
Laser-Cut and Bent Chassis Supports
Sheet metal fabrication handles volume production very well. Laser cutting and bending create chassis supports quickly and cheaply. Tooling costs are low to moderate. Setup takes moderate effort. Cycle times are fast. For runs of 500 to 5,000 units, sheet metal is often the most cost-effective choice. The material waste is lower than CNC because you can nest parts on a sheet. Tolerances are reasonable at ±0.1 to 0.5 mm. That is not as tight as CNC, but it works for many frame applications. Sheet metal fits nicely into an automated production line. Once programmed, the machines run with little human help. This production line automation cuts labor costs and keeps quality consistent. When you need hundreds of chassis supports, sheet metal delivers reliably. The fabrication process scales well from prototypes to full production.
Injection-Molded Plastic Brackets and Covers
Injection molding changes the cost picture completely. The tooling is expensive. A steel mold can cost $2,000 to $50,000 or more. At 100 parts, that $10,000 mold adds $100 to each part. But at 10,000 units, the mold cost drops to just $1.00 per part. The unit cost falls to pennies. Cycle times are very fast. The process handles high automation well. That is why injection molding dominates at volumes above 5,000 units. Plastic brackets, covers, and housings come out consistently. The material choices include nylon, ABS, and polycarbonate. Each offers different balances of strength, impact resistance, and cost. The sweet spot for injection molding is 1,000 units and above. Below that, the tooling cost hurts. But once you commit to high volume, nothing beats it for low per-part cost. An automated production environment with injection molding machines runs with minimal labor per part.
Volume Band Recommendations
| ボリュームバンド | 最も費用対効果の高い | 理由 |
| 1-50 | 3Dプリント、CNC | Minimal NRE; fast learning. |
| 50-500 | CNC、板金 | Repeatability without high tooling risk. |
| 500-5,000 | 板金、橋梁成形 | Transition zone: repeatability starts to pay off. |
| 5,000件以上 | 射出成形、ダイカスト | High NRE is fully amortized; speed is king. |
From a practical perspective, companies like NOBLE bring deep expertise across all these processes. NOBLE, a leading manufacturing company in China, helps clients choose the right method for each AMR structural part. Their experience with CNC, additive manufacturing technologies, sheet metal, and injection molding ensures efficient prototyping and mass production.
Designing AMR Structural Parts for Performance
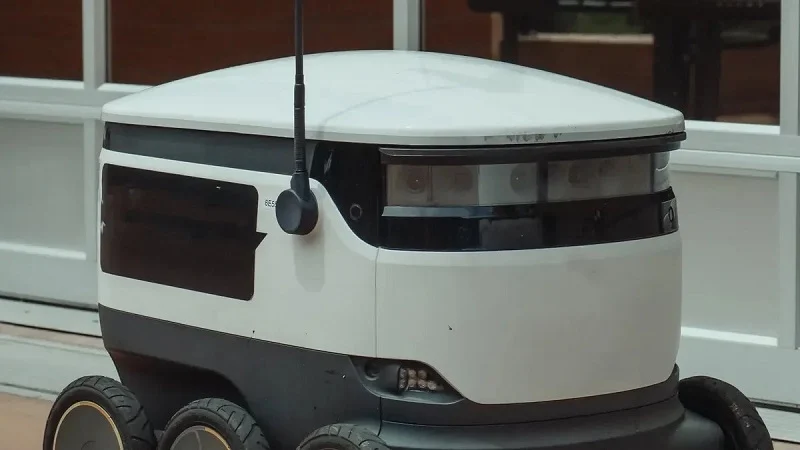
Good design turns a working part into an efficient one. Every gram you save and every feature you add changes battery life, sensor accuracy, and maintenance costs. The right choices early on also make manufacturing much smoother.
Weight Optimization for Battery Efficiency
Battery weight drives AMR range. A heavier robot needs more power to move. That means bigger batteries, which add even more weight. Breaking this cycle starts with smart structural design.
Use of ribbing, pocketing, and honeycomb structures
Ribbing adds stiffness without adding bulk. Think of it like the ridges on a plastic bottle cap. A flat panel might need to be 8 mm thick to resist bending. Add a few ribs, and you can drop that to 4 mm. The strength stays the same. The weight drops by almost half. Pocketing works the same way on CNC-machined parts. You carve out material where stress is low. The part keeps its outer shape, but the inside is hollow. Honeycomb structures take this further. They are great for covers and housings. The challenge is matching the design to the process. Ribs fit injection molding perfectly. Pocketing works in CNC and 3d printing. Honeycomb patterns are possible with additive manufacturing technologies. Each process has its own limits. Talk to a partner like NOBLE early. They can tell you which features are practical. Their design for manufacturability support saves time and money.
Strength vs. Material Cost
Lighter materials cost more per kilogram. Carbon fiber saves weight but raises the budget. Aluminum 6061 hits a sweet spot. It is strong, light, and affordable. For high-stress parts, you may need steel. But steel is heavy. The smart move is hybrid designs. Use steel only at load points. Use aluminum or plastic everywhere else. This keeps the weight down without breaking the bank. Manufacturing process matters here too. Injection molding lets you mix materials in one part. Overmolding adds a soft grip or seal. 3d printing lets you vary density inside the same part. These engineering tricks save grams in real applications.
Thermal Management and Environmental Sealing
AMRs run for hours. Motors, batteries, and electronics generate heat. Dust and moisture are everywhere in warehouses. Good design handles both problems.
Heat Sinks and Ventilation Integration
Heat sinks pull heat away from hot components. The best ones have fins that increase surface area. You can machine them from aluminum or print them with conductive polymers. Ventilation channels let air flow through the chassis. A well-placed fan moves hot air out. The trick is making room for these features without adding size. Integration matters. A motor mount that doubles as a heat sink saves space. That kind of dual-purpose engineering is common in advanced systems. Every gram you save on cooling parts goes straight to payload or battery.
Sealing sensor mounts against dust and moisture
Sensors are the eyes of the robot. A dirty lens means bad data. Sealing keeps dust out. O-rings and gaskets work well. So do overmolded seals. The design needs a groove or lip for the seal to sit in. This adds a small amount of complexity to the part. But it saves big on maintenance. For outdoor AMRs, the sealing needs are tougher. You need IP65 or higher ratings. That means tight tolerances on every mating surface. A partner with CNC expertise can hold those tolerances. NOBLE, a leading manufacturing company in China, provides that precision. Their professional machining expertise ensures seals work the first time.
Serviceability and Modular Assembly
Field maintenance keeps robots running. Downtime costs money. Parts that are hard to reach or replace create headaches.
Quick-release fasteners and cable routing channels
Bolted joints are reliable but slow. Quick-release fasteners let you swap a part in seconds. Quarter-turn fasteners and spring clips are common choices. Cable routing channels keep wires tidy. A channel cut into the frame guides the cable. It stops abrasion and makes tracing easy. These features add a bit of machining time. But they save hours in the field. Good production line automation can handle these details. Programming the CNC to cut a channel takes a few extra lines of code. The payoff is big in serviceability.
Designing for disassembly in field maintenance
Snap-fit parts break when you take them apart. Screws do not. Design every joint to be opened at least three times. Use stainless steel hardware to avoid corrosion. Label each connector. This sounds simple, but many designs skip it. A modular assembly lets you replace one part without removing everything. Battery housings should slide out. Sensor brackets should pop off. These decisions make material handling smoother. They also reduce inventory needs. You stock a few common parts instead of many custom ones. Safety improves too. A tech can swap a faulty sensor in two minutes instead of twenty.
Materials for AMR Structural Parts
Choosing the right material changes weight, cost, and how you make the part. Each making method works best with some materials. The choice also decides how long the part will last.
Aluminum Alloys: Lightweight and Machinable
Aluminum works in many robot uses. Two grades stand out.
6061-T6および7075
6061-T6 is the usual choice for most parts. Its yield strength is 276 MPa. Its fatigue strength is 97 MPa at 500 million cycles. That is good for chassis and brackets. For heavier loads, 7075-T6 has a yield of 503 MPa. That helps for parts under high stress. The downside is cost. 6061-T6 costs $2 to $5 per kg. With CNC machining, each part costs $50 to $500. This making method works well for small batches.
| プロパティ | 6061-T6 | 7075-T6 |
| 降伏強さ | 276 MPaで | 503 MPaで |
| 疲労強度 | 97 MPaで | 159 MPaで |
| 抗張力 | 310 MPaで | 572 MPaで |
Anodizing and other surface treatments
Anodizing protects each aluminum part from wear. Type II anodizing makes a layer from 0.0001 to 0.001 inches. Type III goes to 0.004 inches and gives better wear protection. But it lowers fatigue strength. For parts that face many cycles, choose Type I. These treatments make the part last longer.
Engineering Plastics: Impact and Cost Benefits
Plastics save weight and cost for each part. They also fight rust without extra help.
Nylon and ABS
Nylon 6/6 costs $1 to $2 per kg. With 3D printing, each part costs $10 to $50. That is much less than aluminum CNC. Nylon can take impacts well. ABS costs less but is not as tough. Both work with additive methods like FDM and SLS. This 3D printing way works well for small runs.
| 材料 | 1kgあたりのコスト | プロセス | 部品あたりのコスト |
| 6061-T6 | 2~5ドル/kg | CNC | 50〜500ドル |
| ナイロン6/6 | 1~2ドル/kg | 3D印刷 | 10〜50ドル |
Aluminum costs ($50–500 per part) are higher than nylon 3D printing ($10–50). Nylon is better for low-cost projects.
Polycarbonate
Polycarbonate is tougher than nylon. It handles impacts well. For uses that need strength, it works in many systems. The 3D printing way for this part uses additive methods.
Composites and Steel for Extreme Conditions
Some uses need very high strength. Composites work for those needs.
Open/closed mold carbon fiber
Carbon fiber gives the best strength for its weight. Open-mold methods make strong parts. Production takes more time. But the results are the best for frames. This making process uses additive technologies. The 3D printing way for each part needs care. These engineering uses call for strong materials.
ステンレス鋼
Stainless steel resists rust. It works for outdoor robots. The making process is CNC or sheet metal work. This part costs more than aluminum. But it lasts longer. For safety parts, it adds reliability.
NOBLE, a top manufacturing company in China, has deep knowledge of these materials. Their advice helps clients choose the right material for AMR body parts. This makes sure the making method fits volume and cost goals.
Partnering with NOBLE for AMR Structural Parts Manufacturing

Comprehensive Metal and Plastic Processing Expertise
CNC machining, injection molding, sheet metal, and 3D printing
NOBLE has all the important ways to make AMR structural parts. Their team does 3D printing, CNC machining, injection molding, and sheet metal work in one place. These methods work for all your needs. For a prototype, 3D printing is fast. For more parts, they use injection molding. An automated line handles large numbers. For chassis, they use sheet metal with laser cutting. They pick the process based on how many parts you need and what material you want. Experts choose the best process and material for each part. They think about how the part will be used. Robots need precise parts. Material handlers need durable parts. The team uses its engineering know-how for every part. Automation cuts costs. It allows making many parts. 3D printing and traditional methods work together for complex parts.
Full-service from design for manufacturability to final assembly
They help with design early. NOBLE looks at your 3D model and suggests ways to make it easier to produce. They round sharp corners. They make thin walls stronger. These small changes save money and stop parts from breaking. The service goes beyond design. NOBLE handles getting materials, machining, finishing, and putting parts together. You get finished parts that are ready to use. This one-stop approach reduces the need to manage many vendors. One team manages everything. For complex AMR builds where parts must fit together well, this support is valuable. The process runs smoothly from start to finish. Tough jobs benefit from this approach.
品質認証:ISO 9001:2015およびISO 13485:2016
Rigorous quality management for precise, consistent parts
ISO 9001:2015 sets the basic quality level. They check each step in the process. They measure size and check surface finish. Records are kept so you can trace parts. If a part fails, you can find its batch. This is important for safety-critical parts. A loose sensor can stop a robot in its tracks. Good quality prevents that. Every part meets the specs. Tough jobs need this reliability. The process gives consistent results every time.
Medical-grade process control applicable to demanding robotics
ISO 13485:2016 adds stricter controls. NOBLE has this certification. This means very high standards for AMR parts. For critical robotics, this standard builds trust. The same process that checks surgical parts checks your motor mount holes. This precision helps the robot navigate accurately. The team follows strict rules. Every part meets high quality standards. The process is documented and controlled. Parts that need this precision benefit a lot.
End-to-End Support for AMR Development
Material selection guidance and design optimization
What material you pick affects cost, weight, and how long it lasts. NOBLE’s engineers help you choose materials. For a light part, try aluminum 6061 or carbon fiber. For impact resistance, use nylon or polycarbonate. For high stiffness, steel may work. The team looks at your load needs and suggests the best material. They design the part for the chosen process. A part for injection molding has even wall thickness. A part for 3D printing has angles that don’t need supports. These changes make production easier. Knowing the process leads to better design. 3D printing gives you unique design freedom. Material choice directly affects the final part.
Single-source accountability from prototype to production
One company does everything. For prototypes, they use 3D printing to make changes fast. When the design is final, they move to CNC or injection molding. NOBLE handles the switch. You don’t need to send files to different shops or check new vendors. The same engineers who worked on the prototype watch over production. This stops problems early. For material handling robots that need to work well every time, this reliability is important. The team is involved from start to finish. One source is responsible for everything. This saves time and lowers risk in choosing materials and making parts.
Picking the right process comes down to volume, strength, and cost. Low-volume complex parts fit CNC machining. High-volume plastic parts suit injection molding. Prototypes and complex geometries work best with additive manufacturing, like polymer 3D printing or composite molding. Durable frames need sheet metal or composite processes. Design choices around weight, thermal management, and serviceability shape which manufacturing method makes sense. Material selection matters just as much. Before choosing, evaluate your required volumes, strength needs, and cost targets. Partner with a manufacturer like NOBLE. Their expertise across metal and plastic processes ensures efficient production of AMR structural parts.
FAQ of AMR Structural Parts Manufacturing
What makes AMR structural parts different from regular robot parts?
AMR structural parts have to deal with flexible navigation and places that keep changing. They must be light so the battery lasts, but also strong enough to handle daily wear. Unlike fixed robots, these parts face constant movement, vibration, and loads that shift. That calls for careful design and the right manufacturing process for each job.
Which manufacturing process works best for low-volume production?
CNC machining is great for low-to-mid volume runs. You get tight tolerances without spending a lot on tooling. For batches under 500 units, this process gives steady quality at costs you can predict. Additive technologies like 3d printing also work well for prototypes. Each method has trade-offs in speed, cost, and material options.
How does 3d printing fit into AMR part production?
3d printing is best at complex shapes and quick changes. FDM and SLS handle brackets, housings, and prototypes well. The technology removes tooling costs, so it is perfect for custom designs. But unit costs stay flat, so 3d printing fits low volumes better than mass production. Many manufacturers use it alongside traditional methods.
When should I choose injection molding over other processes?
Injection molding wins at volumes above 5,000 units. The upfront tooling cost is high, but per-part costs drop a lot. Plastic brackets, covers, and housings come out fast and consistent. For high-volume production, this process beats CNC and 3d printing on cost. Below 1,000 units, the math rarely works.
What materials work best for AMR structural parts?
Aluminum 6061-T6 gives a great strength-to-weight ratio for chassis and brackets. Engineering plastics like nylon and polycarbonate save weight and resist impact. Carbon fiber composites deliver the most strength for demanding applications. Stainless steel suits outdoor robots that need to resist rust. Material choice affects both the manufacturing method and final performance.
Can additive manufacturing handle structural loads?
Yes, if you design it carefully. Polymer 3d printing makes strong brackets when layer orientation lines up with stress directions. SLS nylon parts show good impact strength. For higher loads, composite molding with carbon fiber gives excellent results. Testing and validation are still a must before using additive parts in critical applications.
How do I optimize AMR structural parts for weight?
Ribbing, pocketing, and honeycomb structures remove material where stress is low. These features work differently across manufacturing processes. Injection molding handles ribs well. CNC machining is great at pocketing. Additive technologies allow complex lattice designs. The goal is saving grams without giving up strength or safety.
Why partner with NOBLE for AMR structural parts?
NOBLE brings deep expertise across CNC machining, injection molding, sheet metal, and 3d printing. Their ISO certifications ensure consistent quality. The team guides material selection and design optimization from prototype to production. As a leading manufacturing company in China, NOBLE helps clients navigate process choices efficiently.





