

A surgical robot part fails, and a patient gets hurt. That is the real problem behind every choice in this field. Precision, biocompatibility, and regulatory compliance are not just big ideas — they decide if surgery works or not.
The market shows that pressure. Grand View Research says the global surgical robotics industry was USD 14.1 billion in 2025, growing at 14.9% CAGR through 2033. Towards Healthcare reports similar momentum: USD 13.79 billion in 2025 and 16.54% CAGR through 2035.
| Source | Market Size 2025 | CAGR |
| Grand View Research | USD 14.1 billion | 14.9% (2026–2033) |
| Towards Healthcare | USD 13.79 billion | 16.54% (2026–2035) |
Engineers and procurement teams face a hard challenge. They must balance manufacturing processes, material choices, and tolerance requirements for surgical robot parts against strict medical standards. One wrong call on a surgical robot component can put an entire system at risk.
Machining Processes for Surgical Robot Parts
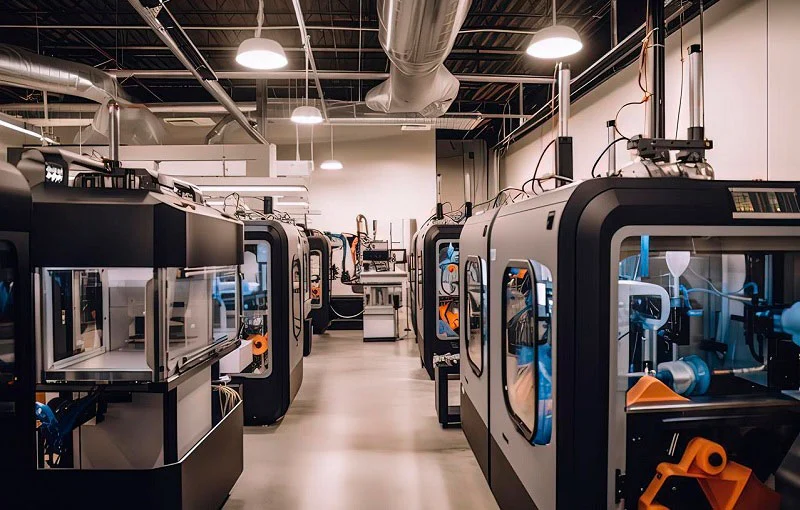
Picking the right method determines if a surgical robot part works the way it was designed. Surgical robots depend on this manufacturing process for surgical robot part manufacturing, giving the accuracy that surgery needs.
Five-Axis CNC Machining
Geometric Accuracy
A five-axis CNC machine cuts a part from many angles in one setup. That single setup is key for surgical-grade manufacturing. The part stays in one reference system, so alignment errors don’t pile up. For medical robots, this means complex shapes stay true to the CAD model. Software controls the orientation shifts, which lowers tolerance stacking. One manufacturer says they can hold tolerances as tight as ±0.020 mm for surgical robot parts. That level of accuracy matters when a component controls a tool inside a patient. These parts must give consistent quality every time.
Surface Finish Control
Surface finish is just as important. A rough surface on a medical instrument can cause friction or trap bacteria. Five-axis machining fixes this by keeping the cutting tool at the best angle for every surface. The tool moves smoothly across curved faces. This makes a cleaner cut and extends tool life. In medical robots, good surface finish cuts down on secondary work.
EDM and Wire EDM
Hardened Materials
Wire EDM gives a clear advantage for parts made from tough materials. It cuts any conductive metal no matter how hard it is. This includes hardened 400 series stainless steel, grades 420 to 440, which medical tools often need. Tungsten and molybdenum cut easily too. The wire never touches the workpiece, so there is no tool pressure to deflect thin sections. This is one of those specialized manufacturing processes that makes hard materials workable for medical robots.
Fine Feature Cutting
For fine features, wire EDM does a great job. It makes sharp corners with minimal radius. It creates long, precise holes that other methods cannot match. No burrs or tool marks remain after cutting. Surface finishes reach as fine as 3 microinches Ra. With slower settings, tolerances can reach ±0.0002 inches. That level of manufacturing precision is vital for high-precision medical robot parts. Parts with complex shapes or small alignment holes benefit from this approach. Accuracy here directly affects patient safety.
Swiss Machining and Laser Processes
Small Intricate Components
Swiss machining is the top choice for small, detailed parts. Medical robots often need tiny shafts, pins, or connectors inside the robotic arm. Swiss lathes feed bar stock through a guide bushing and support the material right at the cutting point. This lets the machine hold tight tolerances on long, thin parts. For high volumes, Swiss machining is efficient and fast.
Micro-Scale Laser Cutting and Welding
Laser processes handle parts too small for regular tools. A focused beam cuts thin metals, tubes, and plastics with minimal heat spread. The edges stay clean with a small heat-affected zone. Laser welding joins tiny components without adding weight. These surgical robot components support the trend toward smaller, less invasive tools.
Additive Manufacturing for Prototypes and Complex Geometries
3D printing plays a supporting role in surgical robot manufacturing. It handles prototypes and complex shapes that would cost too much to machine. Engineers test designs with printed parts before committing to production. This manufacturing technology helps validate complex shapes. Some end-use parts with organic shapes also benefit from this approach. For precision machining operations, 3D printing creates near-net shapes that go to CNC for final tolerances. Medical robot parts made this way combine design freedom with subtractive accuracy. The materials used here must also meet medical standards.
Additive and Sheet Metal in Surgical Robot Manufacturing
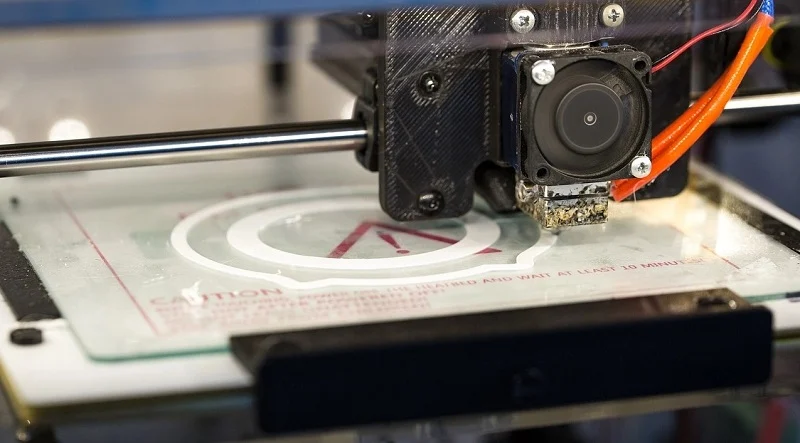
3D Printing for Surgical Robot Parts
Rapid Prototyping
Speed is important when you keep changing a new tool design. 3d printing lets engineers hold a real part in days, not weeks. This quick feedback finds design problems before costly tooling is made. For surgical robot parts, a printed prototype can check fit and feel early. Printed prototypes do not replace final machined parts — they just make the path to them safer.
Complex Geometries
Some shapes are almost impossible to cut with a spinning tool. 3d printing builds them layer by layer instead. Inside channels, lattice structures, and organic curves all become possible. In a real way, this design freedom helps medical robots lose weight without losing stiffness. The same 3d printing workflow also makes near-net shapes that later go to CNC for final precision.
Sheet Metal Fabrication
Laser Cutting and Bending
Not every surgical robot component needs micron-level accuracy. Frames, brackets, and mounting plates often start as flat sheet stock. A laser cuts the outline, then a press brake bends it into shape. This manufacturing process is fast and repeatable at volume. It keeps costs down for the larger structural pieces of a surgical robot.
Welding for Frames and Chassis
After bending, those pieces get joined. TIG welding and spot welding both work well for thin-gauge frames. A rigid chassis keeps the arm stable during surgery, so weld quality directly affects performance. Fixtures hold alignment during the weld, which protects the overall geometry. Post-weld stress relief may be needed for critical assemblies.
Casting of Aluminum and Steel
Structural Metal Parts
Casting pours molten metal into a mold to form a shape. It suits bulky structural parts like bases and joint housings. Aluminum casts light and resists corrosion. Steel casts strong and takes heavy loads. Both give designers freedom for ribs and bosses that would be costly to machine from solid stock.
Cost-Effective Production
Tooling costs money up front, so casting pays off at higher volumes. Per-part cost drops as quantities climb. That makes it a smart fit for medical robot parts produced in steady runs. Machining then finishes the critical surfaces. This blend of casting and machining balances cost against the tight tolerances surgical work demands.
Design Considerations for Surgical Robot Parts
Minimally Invasive Design
Miniaturization and Articulation
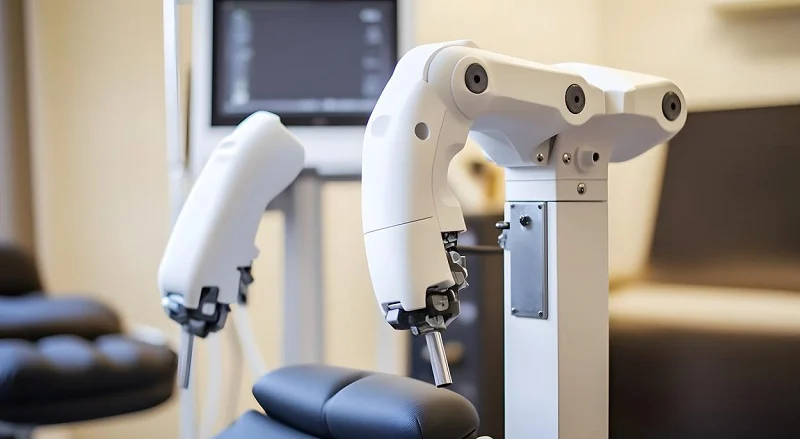
Smaller parts are key for minimally invasive work. Surgical robot parts must be small but strong. They need inner channels for fluids, optics, or cables. CNC micro-machining allows this. Articulation adds more complexity. Precision gearboxes and bearing housings with exact alignment reduce backlash. This keeps positioning repeatable, which is important for haptic feedback in master-slave systems.
Medical robots rotate 360 degrees and copy natural hand movements with less trembling. This ability helps in tight spaces inside the body. Cable-driven flexible tools replace lever-arm systems, so motion occurs inside the body. Actuation cables about 110 microns wide must go through channels only 40 microns wider. That requires exact anchoring and tight clearances.
Sterilization Compatibility
Every part must handle repeated sterilization without breaking down. Steam autoclave, gamma irradiation, and VHP are common methods. Choosing the right material is important. Titanium, PEEK, and 316LVM stainless steel work well under these conditions. Autoclave-resistant threaded couplings and surface finishes with Ra ≤0.2 μm for sliding surfaces also help. Biocompatibility is directly related. A part that fails under heat or chemicals can release particles into a patient.
Structural Integrity
Load-Bearing Components
Load-bearing parts in medical robots must handle strong forces. Crossed roller bearings manage radial, axial, and moment loads all at once. They provide great rigidity for arm joints and rotating bases. Thin-section bearings save weight while supporting loads from many directions. In practice, the bearing type you choose shapes the whole arm design. Miniature stainless steel bearings work well in catheter drives and endoscope articulation.
Fatigue Resistance
Repeated loading wears parts down over time. Fatigue testing usually runs 5–10 million cycles at loads that match real use. Forged parts resist fatigue better because grain flow follows the part shape. A forged hip stem lasts longer than a cast or machined one. Specialty stainless steel gives high strength at lower cost. Full ceramic bearings resist rust and need no lubrication, making them good for MRI-compatible medical robots.
Design for Manufacturability
Tolerance Stack-Up Analysis
Tolerance stack-up decides if an assembly works. Small errors add up across parts that fit together. A single setup on a five-axis machine reduces stacking because the part stays in one reference frame. Designers should model worst-case and statistical stacks early. This finds problems before tooling is cut.
Feature Accessibility
Tools must reach every feature. Deep pockets, undercuts, and internal channels can block cutters or leave marks. Swiss machining works well for small intricate parts. Wire EDM makes sharp corners and long precise holes without burrs. Designers who plan tool access early avoid extra steps and keep quality high.
Materials for Surgical Robot Parts
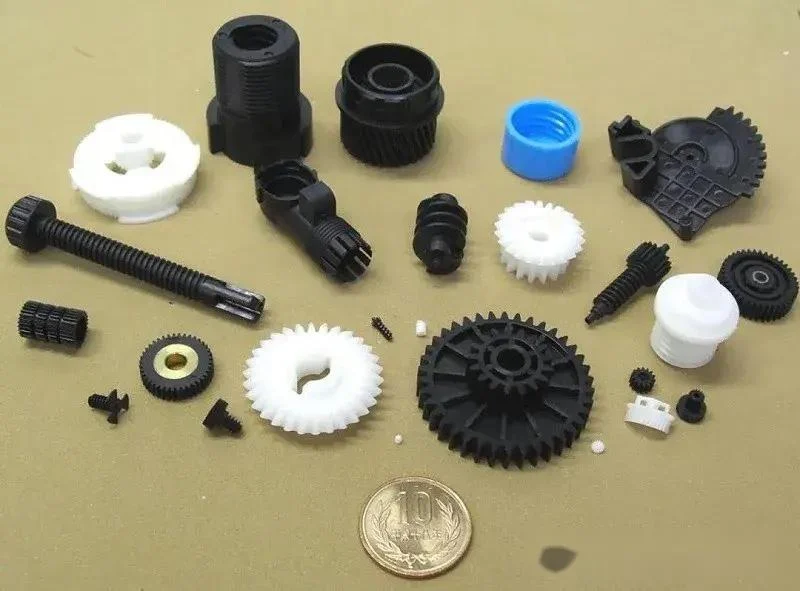
The material you pick decides how a part works inside the body, under heat, and after thousands of cycles. Pick the wrong one, and the problem shows up during surgery. That is why biocompatibility, mechanical needs, and sterilization all matter together.
Metals
Titanium Alloys
Titanium is the top choice for parts that go inside the body or carry heavy loads. Its TiO2 surface helps bone grow directly onto it without soft tissue in between. The oxide layer stays stable in body fluids, so metal ions barely leak out over decades. Ti-6Al-4V has a tensile strength of 895–1,100 MPa and a specific strength of 202–248 MPa·cm³/g. That is as strong as steel but about 45% lighter. Titanium is also 4–5 times stiffer than bone, while stainless steel is about 10 times stiffer. This closer match puts less stress on nearby tissue. Medical robots like the da Vinci Surgical System often use titanium for these reasons.
Stainless Steel Grades
Stainless steel works for many surgical uses at a lower cost. Grade 316L resists rust well and handles many autoclave cycles, so it is common for tools, needles, and non-implanted parts. Its tensile strength is 485–580 MPa, and fatigue endurance is 200–250 MPa at 10⁷ cycles. The 316LVM type resists corrosion even more for short-term implants. Stainless steel is about 10 times stiffer than bone, so it works better for rigid structural parts than for bone contact. For joint housings and rotating connectors that face constant stress, stainless steel and titanium both beat aluminum in fatigue life.
Aluminum Alloys
Aluminum alloys like 7075-T6 give high specific strength (203 MPa·cm³/g) at low weight. Tensile strength reaches 570 MPa. But aluminum is mostly not used inside the body because of toxicity concerns. It may show up in external braces and non-critical hardware. In medical settings, aluminum is okay for external use, but it can pit and needs protective coatings. For surgical robot parts that never touch tissue, it remains a useful option.
Plastics
PEEK and PEI
PEEK is the best polymer for load-bearing parts in surgical robots. It survives over 3,000 sterilization cycles at 134°C, has an elastic modulus close to human bone, and does not block X-rays. That radiolucency helps with imaging during surgery. PEI (Ultem) handles hundreds of cycles with steam, gamma, and EtO. PPSU (Radel) lasts over 1,000 autoclave cycles at 134°C, but it has limited chemical resistance compared to PEEK. These high-performance polymers meet ISO 10993-1, the risk-based biocompatibility standard that replaced older USP Class VI rules.
PTFE and Fluoropolymers
PTFE is chemically inactive and very biocompatible. It resists EtO and gamma radiation but can break down under high-temperature sterilization. Its low friction makes it great for bearings, seals, and catheter linings. The trade-off is that it creeps under load and is hard to bond. Other polymers fill specific roles. Polycarbonate works for clear housings that only need a few sterilization cycles. Nylon handles bearings and gears in low-load uses. Acetal (POM) suits precision gears and sliding parts. Silicone elastomers serve soft robotic actuators and flexible joints that are safe for the body. Each choice links back to part function and sterilization exposure.
Ceramics
Alumina and Zirconia
Alumina and zirconia ceramics offer excellent wear resistance and hardness. They resist rust and keep their shape through many sterilization cycles. Zirconia is tougher than alumina, so it works better for load-bearing surfaces that move. Alumina is best where hardness and chemical stability matter most. Both materials appear in bearing surfaces and precision parts where metal wear bits would be unacceptable.
Biocompatibility and Wear Resistance
Ceramics are naturally safe for the body and do not release metal ions. That makes them attractive for long-term implantable surgical robot parts. Their wear resistance makes parts last longer in high-cycle uses. The downside is they are brittle. Careful design around stress points is needed. From a practical view, ceramics work best when paired with flexible mounting that absorbs shock loads.
Material choice and certification directly link to material properties and performance. Every choice must meet biocompatibility, sterilization compatibility, manufacturability, regulatory paperwork, and supply chain stability. That is the full picture for surgical robot parts.
Tolerances and Surface Finishes for Surgical Robot Parts
Dimensional Tolerances
Critical Feature Tolerances
The tolerances you choose decide if a surgical robot part moves the same way every time or drifts during surgery. For medical devices, normal size tolerances go from ±0.025 mm to ±0.127 mm. That base range gets tighter for moving joints and surfaces that mate together.
| Precision Level | Typical Tolerance Range |
| Standard machining | ±0.005″ (0.13 mm) |
| Precision machining | ±0.001″ to ±0.002″ (0.025–0.051 mm) |
| High precision (reamed holes) | ±0.0005″ (0.013 mm) |
| Ultra-precision | ±0.0002″ (0.005 mm) |
Surgical robot parts usually need high to ultra-precision limits. This keeps motion safe and repeatable. Ultra-precision work requires special equipment, so it costs more and takes longer.
GD&T and Inspection
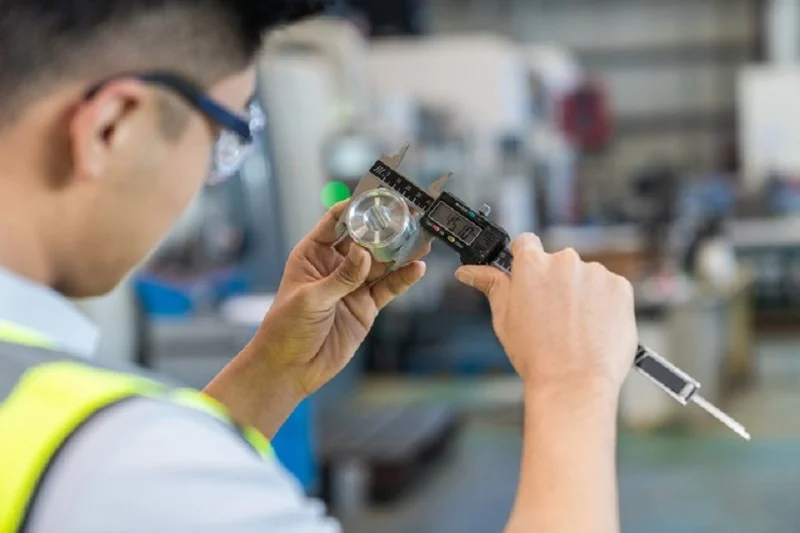
GD&T turns what a part must do into numbers you can measure. Position tolerance with Maximum Material Condition gives extra tolerance as features move away from MMC. This makes sure parts fit together while lowering manufacturing cost. Location controls like true position create round tolerance zones, which work better than rectangular coordinate tolerancing. Orientation controls such as perpendicularity and angularity keep the right angles at assembly interfaces. Material Condition Modifiers (MMC, LMC, RFS) let geometric tolerances change with the actual feature size. These tools directly make sure pivot points, mounting holes, and mating surfaces meet repeatability, safety, and assembly reliability needs. Inspection then checks those callouts with CMM and optical methods.
Surface Finish Requirements
Ra Values and Function
Surface roughness affects how clean a part gets, how much friction it has, and the risk of biofilm. Different surfaces need different Ra targets.
| Surface Type | Recommended Ra (µm) | Process |
| Surgical instruments (cleanability) | 0.4–0.8 | Passivation |
| Articulating surfaces (ultra-smooth) | <0.05 | Not specified |
| Bone-contacting zones | 3–6 | Not specified |
General surgical instruments with Ra above 0.8 µm carry biofilm risk and should not be used. Electropolishing lowers Ra by 30%–50%, reaching 0.4–0.8 µm on CNC-machined stainless steel parts. It also removes tiny burrs and builds a chromium-rich passive layer.
Polishing and Passivation
Mechanical polishing lowers Ra a little but may leave micro-scratches. Chemical passivation removes free iron without improving Ra. Electropolishing does both — it smooths the surface and builds a chromium-rich passive layer.
ASTM F86-21 covers surface preparation and marking of metallic implants, including passivation to remove contaminants and form a protective oxide film. Surface finish must be validated after all post-processing steps — passivation alters surface characteristics.
Cleanliness and Sterilization
Cleanroom Manufacturing
Cleanroom operations must follow ISO 14644-1 particle limits and FDA 21 CFR Part 820 quality requirements. ISO 7 (Class 10,000) works for components with direct patient contact before terminal sterilization. Air changes run 60–90 ACH with HEPA filtration at 99.97% efficiency for 0.3 µm particles. Maximum particle count stays at 352,000 particles ≥0.5 µm per cubic meter at operational state. Environmental monitoring includes airborne particle counting, microbial testing, and HEPA filter integrity checks.
Cleaning Process Validation
Terminal sterilization methods — EtO, gamma, and autoclave — cannot remove embedded particles from machining. EtO gas penetration is blocked by particle accumulation. Gamma radiation can be physically shielded by particulates. Autoclave heat and steam cannot dislodge trapped particles. These particulates can shield microorganisms from sterilizing agents, producing non-sterile products despite a validated cycle. Bioburden must meet ISO 11737-1 limits before sterilization. Cutting fluids, particles, and machine lubricants must be evaluated under ISO 10993-1 biological risk assessment.
Compliance and Quality Assurance for Surgical Robot Parts
Compliance keeps surgical robot parts safe for patients. A good quality system does more than check boxes. It protects lives.
Design engineers work within limits set by FDA rules, ISO 13485 quality management systems, and biocompatibility standards like ISO 10993. Every design choice—picking materials, setting surface finish, assigning tolerances—affects both how easily a part can be made and whether it gets approved.
These rules shape every part that goes into surgery.
ISO 13485 and Medical Standards
Quality Management Systems
ISO 13485 sets the basic rules for medical device quality. Suppliers of surgical robot parts must follow this system. The standard covers everything from getting materials to final release. It keeps quality the same across every batch. A supplier with this certification shows real dedication to surgical-grade manufacturing. They know the rules that keep patients safe.
Risk Management and Traceability
ISO 14971 handles risk across the whole product lifecycle. Manufacturers must find problems during design. They test parts in realistic surgical situations before production starts. Traceability lets you follow a part from raw material to finished product.
| ISO 13485 Requirement | What It Means for Surgical Robot Parts |
| Risk Management | Risk-based methods apply across the whole product lifecycle. A special risk management file must exist for each device type. |
| Traceability | Records must link device IDs to production batches, component lots, and distribution records. You must be able to rebuild the full product history. |
If a supplier reports a bad material lot, traceability records let you find the exact robots affected. This keeps patients safe and stops recalls across the whole market.
Inspection and Testing
CMM and Optical Inspection
Inspection proves the part matches the design. A CMM checks dimensions with high precision. It makes sure critical features stay within tolerance. Optical inspection finds surface flaws. Scratches or burrs can cause problems during patient use. For medical robot parts, this level of checking is normal. Every part gets a careful look before it moves forward.
Material Certifications
Every material batch needs a certificate. A Certificate of Conformity links the lot back to the mill. For parts touching the body, ISO 10993 test results prove safety. Material certifications are the paper trail that shows compliance. They are a basic part of good manufacturing.
Documentation and Traceability
Device History Records
Documentation holds the quality system together. A Device Master Record tells you how to build the device. A Device History Record proves you built it correctly.
| DHR Element | Required Content | Traceability Link |
| Device identification | Part number, revision, serial/lot number | Links to DMR drawing revision |
| Component records | Supplier, lot number, CoC reference | Links to incoming inspection record |
| Production records | Route card, operation sequence, operator IDs | Links to work instructions revision |
| Inspection records | Inspection report ID, results, pass/fail, inspector | Links to drawing revision and calibration record |
In medical robots, the DHR connects everything. If a problem happens, the DHR is the first place to look. ISO 13485 is clear about these records. Clause 7.5.9 requires traceability. Clause 7.5.1 controls production. A good DHR protects patients during surgery.
Supplier Quality Management
The last piece is supplier quality management. You need an Approved Supplier List. Regular audits keep partners accountable. Strong supplier agreements manage risk. You must trust your partners to follow the rules. For surgical robot part manufacturing, good suppliers build better medical robots. They help deliver precision where it matters most.
Molded and Extruded Components for Surgical Robot Parts
Fluid Path Tubing
Extrusion Processes
Extrusion makes the long hollow tubes that carry fluids inside a surgical robot. You push melted material through a die, and it comes out as one continuous shape. For surgical robot parts, microbore extrusion makes tiny tubes with inner diameters under a millimeter. Multilumen extrusion puts several channels inside a single tube. Each channel could carry a different fluid or cable. That design keeps the robot arm neat. PEEK extrusion handles high heat and holds its shape through repeated sterilization.
Material Selection
The material must stay flexible but strong. It has to survive sterilization without breaking down. Lubricious tubing lowers friction when the tube slides inside a catheter delivery system. That helps the robot move tools with precision. Reinforced shafts have a braid inside the wall for extra strength. For steerable catheters, the material must bend at the tip when control wires pull it. Good materials directly affect how the robot performs during surgery. The right materials also make sterilization easier and more reliable.
Molded Parts and Seals
Custom Reusable Components
Injection molding makes parts for robot housings and control handles. Medical robot parts need tight tolerances. Overmolding puts a soft grip layer over a hard core. Micromolding makes tiny seals that fit inside small joints. These reusable parts get washed and sterilized after every procedure. The mold tooling costs more upfront, but each part costs less at volume. Medical robots depend on these consistent parts for reliable motion. This process supports efficient surgical robot manufacturing.
Disposable Components
Some parts touch the patient and then get thrown away. Surgical drapes cover the robot arm to keep the field sterile. Sterile draping film protects from contamination. Insulation sheaths go over wires and tools. Metal replacement components made from molded plastic save weight and cost. These disposable parts reduce infection risk. They leave the mold fully formed with no extra processing. Quality checks happen at the press to catch defects promptly.
High-Volume Production
Molding Efficiency
Once the mold is made, injection molding runs fast. A multi-cavity mold produces several parts each cycle. That speed matters for medical robots in high demand. Lines run twenty-four hours a day with minimal operator help. The process wastes very little material because you reuse the scrap. A steady manufacturing rhythm keeps the supply chain moving. Medical robots rely on this output to meet hospital schedules.
Quality Control
Molding needs strict quality control. Each cavity wears over time and changes part dimensions. Medical robots depend on stable tooling for consistent output. Statistical process control catches drift before parts go out of tolerance. Visual inspectors check for flash and short shots. Material lots get tested for consistency. These steps ensure every batch matches the last. Reliable parts protect patients during surgery.
Choosing a Manufacturer for Surgical Robot Parts
Picking the right partner for surgical robot part manufacturing is a big decision. The wrong choice can cost you time, money, and maybe even a recall. So how do you tell the best from the rest?
Manufacturing Capabilities
Equipment and Technology
A serious partner owns the right machines. Look for multi-axis CNC systems, EDM equipment, and CMM inspection tools. These let them hit tight tolerances on complex surgical robot parts. They should also offer one-stop capabilities — machining, finishing, and quality control under one roof. That saves you from juggling multiple vendors.
From a practical view, a manufacturer’s technical know-how in advanced manufacturing and robotics is key. Experience with robotic surgical systems matters because these systems are complex and need coordinated skills. Advanced capabilities like automation, laser machining, and cell-based manufacturing are a must for complex components.
Medical Device Experience
Proven experience with surgical robot parts is a must. Ask for examples of intricate, tight-tolerance prototypes they have delivered. A partner who knows medical robots understands the stakes. They also need expertise across materials like SS630, SS316, AL7075-T6, PEEK, and PEI. NOBLE, a leading manufacturing company in China, brings exactly this kind of professional machining expertise. Their team helps clients move from prototyping to mass production efficiently.
Quality and Compliance
Certifications and Audits
Certifications tell you a lot. ISO 9001 and ISO 14001 show a management system suited to the surgery robotics sector. ISO 13485 goes further — it is the gold standard for medical device quality. Regular audits keep partners honest. A supplier with these credentials shows real dedication to surgical-grade manufacturing.
Continuous Improvement
Good manufacturers never stop improving. They track defects, analyze root causes, and refine processes. Statistical process control catches drift before parts go out of tolerance. This mindset protects patients during surgery. Ask potential partners how they handle corrective actions and whether they invest in new technology.
Cost, Quality, and Lead Time
Total Cost of Ownership
The cheapest quote often costs more later. Think about total cost of ownership — inspection, rework, downtime, and compliance risk. A partner with strong quality systems reduces hidden costs. For medical robot parts, reliability beats a low price every time.
Scalability and Supply Chain
Your partner must scale with you. Can they handle a prototype run and then ramp to high volume? Supply chain resilience matters too. A stable network of material suppliers keeps production moving. Here is a quick checklist for evaluating partners:
- Equipment: precision CNC, EDM, and CMM systems
- Technology: one-stop machining, post-finishing, and quality control
- Experience: proven surgical robot parts and tight-tolerance prototypes
- Materials: SS630, SS316, AL7075-T6, PEEK, PEI expertise
- Finishing: passivation for stainless steel, anodization for aluminum
- Quality: dimensional checks and advanced inspection tools
NOBLE checks these boxes. Their precision machining and assembly services help clients complete projects faster. For surgical robot parts, that kind of partner makes all the difference.
NOBLE: Partner for Surgical Robot Part Manufacturing

Metal and Plastic Processing
CNC and Swiss Machining
NOBLE makes surgical robot parts from both metal and plastic. That means you do not need to use different suppliers for different materials. Their shop has advanced CNC machines and Swiss lathes. This mix matters. A rigid joint housing and a tiny actuation pin need very different setups. One partner covering both shortens the path from drawing to finished part. From a practical view, this is where precision becomes a real machine ability, not just a word.
Plastic Injection Molding
Plastic injection molding covers the other half of the work. Housings, seals, disposable draping parts, and fluid path parts all come from the press with repeatable sizes. Overmolding and micromolding handle the small, detailed pieces that medical robots need. Tooling is made in-house. That keeps the feedback loop short when a design changes.
Certifications and Quality
ISO 9001:2015
ISO 9001:2015 sets the basic management system. It shows there are written processes, controlled suppliers, and measurable improvement. For buyers, that means predictable output from batch to batch.
ISO 13485:2016
ISO 13485:2016 goes further. It speaks the language of medical devices. It requires risk-based thinking, traceability, and a quality system built for surgical use. Together, these two certifications tell you the shop can serve both industrial and medical customers without cutting corners.
| Certification | What It Covers |
| ISO 9001:2015 | General quality management system |
| ISO 13485:2016 | Medical device quality management system |
End-to-End Services
Design for Manufacturing
NOBLE’s team reviews your design before cutting the first chip. They flag features a cutter cannot reach. They point out tolerances that raise cost without adding function. They also note material choices that fight the sterilization cycle. This early input saves rework later.
Assembly and Packaging
The service list does not stop at production. Assembly, inspection, and packaging happen under one roof. That way parts arrive ready for the next step. This continuity protects quality and shortens lead times. For surgical robot parts going into surgery, fewer handoffs mean fewer chances for error.
Choosing the right process, material, and tolerance for surgical robot parts is a big deal. It decides whether a procedure goes well. Following ISO 13485 is not a choice either. It is the basic rule for every medical robot parts supplier.
You also need a partner who understands both the technical side and the rules side. That mix is hard to find. In the future, 3d printing, smart materials, and more automation will change surgical robots. So check your partners using these points. Then contact NOBLE for your surgical robot parts needs.
FAQ of Surgical Robot Part
What tolerances can surgical robot parts hold?
Surgical robot parts usually need high to ultra-precision limits. Standard machining hits ±0.13 mm. Ultra-precision work reaches ±0.005 mm. Critical features need these tight limits. This keeps motion safe and repeatable during surgery.
Which materials work best for surgical robot parts?
Titanium alloys give high strength at low weight. Stainless steel costs less and handles autoclave cycles well. PEEK lasts through over 3,000 sterilization cycles. Ceramics like zirconia resist wear very well on moving surfaces inside the body.
What certifications should a surgical robot parts supplier have?
ISO 13485:2016 is the top standard. It requires traceability and risk-based thinking. ISO 9001:2015 shows general quality control. Both certifications show a real commitment to surgical-grade manufacturing and patient safety.
How does sterilization affect surgical robot parts?
Steam autoclave, gamma irradiation, and VHP are common methods. Parts made from titanium, PEEK, and 316LVM stainless steel handle these conditions well. They must survive repeated cycles without breaking down or releasing particles into patients.
Is 3D printing used for surgical robot parts?
Yes, but mostly for prototypes and complex shapes. Engineers test designs before production this way. Some end-use parts with organic shapes also benefit. Near-net shapes often go to CNC for final precision.
What makes surgical robot parts different from regular machined parts?
They need tighter tolerances and materials safe for the body. Surface finishes must stop bacteria from growing. Manufacturing follows ISO 13485 quality systems. Every part can be tracked from raw material to finished product.
How do you choose a manufacturer for surgical robot parts?
Look for ISO 13485 certification and medical device experience. Check their equipment — five-axis CNC, EDM, and CMM tools. A partner who offers one-stop services cuts down on handoffs. This protects quality through the whole process.






