
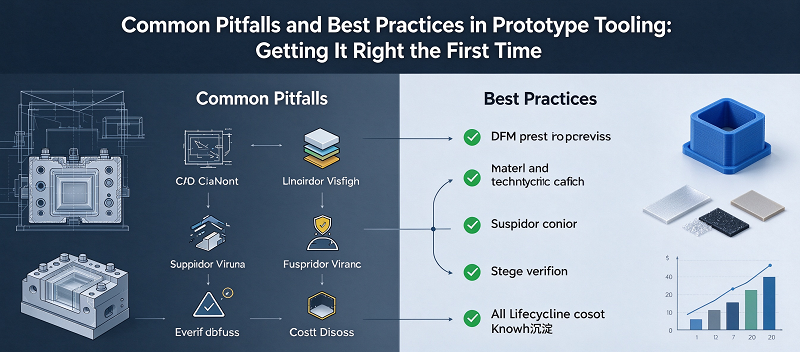
Prototype Tooling is the key bridge between “drawings” and “mass production.”
It produces real parts that can be used for assembly, functional verification, and small-batch trial production at a relatively low cost and in a shorter cycle, allowing the team to discover and correct design flaws before investing in expensive mass production molds.
Data shows that over 70% of the problems in product development originate from the early design stage, and prototyping tools precisely expose these issues at the lowest cost.
However, in actual projects, situations such as “repeated rework of prototype parts, frequent modification of molds, and continuous cost overruns” are not uncommon.
The main reason for this is not that the technology fails to achieve it, but rather that several common pitfalls have been fallen into.
This article breaks down these misunderstandings from three dimensions: design, materials, and suppliers, and provides practical best practices that can be implemented from CAD to mass production.
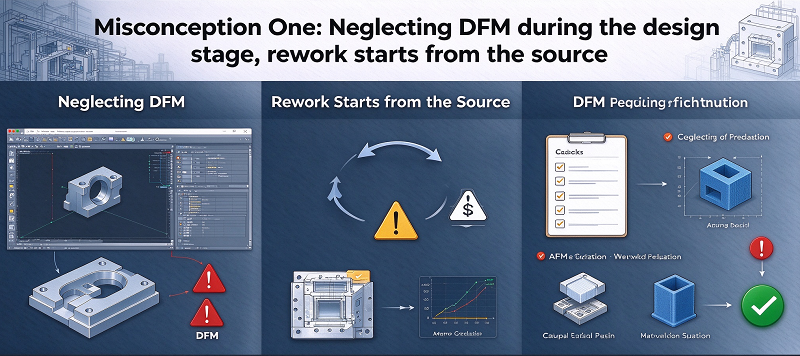
Wanopvatting Een: Neglecting DFM during the design stage; rework starts from the source
DFM is the dividing line for whether a prototyping tool can get it right the first time.
Each round of rework in the prototype stage means rescheduling production, re-injection molding, and re-verification, and the cycle is often extended by weeks.
More importantly, DFM actually determines the cost ceiling of the entire project – a small change at the source may only take a few minutes, but it can save the cost of redoing the entire mold.
The following three high-frequency design issues are the main sources of prototype rework.
Ignoring the draft Angle leads to mold jamming
The demolding of plastic parts requires a sufficient draft Angle (generally 1°to 3°).
If the slope is not reserved during the design, the prototype mold is very likely to scratch the surface of the parts or even get stuck when it is ejected. In mild cases, the mold needs to be repaired; in severe cases, the entire set needs to be redone.
Particular attention should be paid to the slope of the inner side, reinforcing ribs, and deep cavity structure, as these parts are most prone to being scratched during demolding.
It is essential to add bevels to all the side walls perpendicular to the parting surface at the CAD stage and ask the mold supplier to check each item one by one during the DFM review instead of taking remedial measures after the mold trial fails.
Uneven wall thickness causes warping and shrinkage
Drastic changes in wall thickness can cause uneven contraction of parts during cooling, resulting in warping, shrinkage marks, and internal stress.
Although these problems can be identified during the prototype stage, each modification means re-molding and verification, and the cost increases exponentially.
When designing, it is advisable to keep the wall thickness as uniform as possible (commonly ranging from 1.5 to 3mm), set rounded corners and gradual changes at the transition points of thickness, and add reinforcing ribs or anti-warping structures to large flat areas to reduce risks at the source rather than leaving the cost of error correction to the later stages.
The tolerance setting is too strict
If the mass production tolerance is directly applied to the prototype parts, it will lead to a sharp increase in mold costs and a decline in the pass rate.
The purpose of the prototype tooling is to verify “shape, assembly, and function”, rather than the final accuracy.
A reasonable approach is to set tolerances at different levels based on the verification targets: be strict at key fit positions and relaxed at appearance and structural positions, leaving the precision to the mass production mold and keeping the cost to oneself.
Excessive pursuit of precision will only make the prototype stage expensive and slow, but it will not bring any substantial benefit to product verification itself.

Misconception Two: The selection of materials and processes is divorced from actual needs
The mold-making process of the prototype tooling (such as soft molds, hard molds, 3D printing molds, etc.) and the selection of forming materials directly affect the credibility of the verification results. If the wrong choice is made, it will be a waste of time to test, and no reliable conclusion will be obtained despite spending money.
The mold-making process determines the cost, lifespan, and cycle of the mold, while the forming material determines the performance and feel of the part. Both must be considered comprehensively and always focus on the question of “what exactly is this prototype to verify?”
Soft molds were mistakenly used in mass production
Silicone molds, epoxy resin molds, and other soft molds have low manufacturing costs and fast cycles, but their lifespan is usually only a few dozen to a few hundred mold cycles, making them suitable for small-batch prototype verification of up to ten pieces.
If it is used to withstand the first batch of trial production or small-batch orders, the mold will soon be scrapped and become even more expensive.
Before making a choice, first clarify “how many pieces to produce and what to verify”: if the quantity is small and only concept verification is needed, choose a soft mold.
Bridge dies are needed for a certain batch or close to mass production.
Make sure that mass production is about to start before investing in hard molds to avoid “overkill” or “overkill”.
Prototype material is inconsistent with the mass production material
The performance data verified with standard PP cannot represent the performance of the final mass-produced material.
When the material performance affects the functional judgment, it is essential to ensure that the prototype stage uses the same grade as in mass production, or at least mark the material differences in the report to avoid subsequent rework due to “goods not matching the description”.
For parts that are sensitive to key properties such as mechanics, temperature resistance, and chemical resistance, material consistency is particularly important; otherwise, the verification results may be misleading.
Underestimate the costs of surface treatment and post-treatment
The prototype also requires post-treatment such as painting, electroplating, embossing, and assembly.
Many projects only calculate the mold cost and neglect the post-processing, resulting in a serious budget overrun.
At the scheme stage, surface grade, post-treatment methods, and quotations should be included in the assessment together in order to make a true total cost judgment.
The closer the surface requirements are to mass production parts, the higher the cost in the prototype stage will be. It is essential to clearly define the surface grade before the project starts to avoid additional requirements in the middle of the process disrupting the budget.
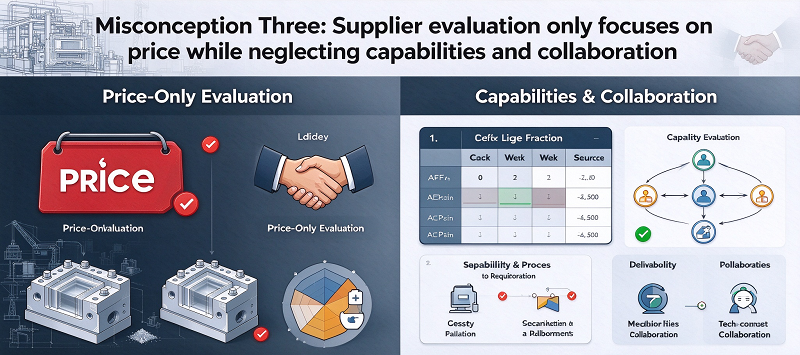
Wanopvatting Three: Supplier evaluation only focuses on price while neglecting capabilities and collaboration
Many purchasers compare the prices of prototype molds as standard parts, choosing the one that is cheaper. As a result, they end up paying a higher price in collaboration.
Prototype tools are highly dependent on the experience and cooperation of suppliers. The hidden cost of choosing the wrong partner is far higher than the saved price difference.
An unsmooth collaboration often means repeated mold modifications, delayed delivery, and even untrustworthy verification results.
The assessment should be made comprehensively from three dimensions: ability, collaboration, and cases, rather than just focusing on the unit price.
Only focusing on quotations while neglecting qualifications and equipment capabilities
Low prices often mean that equipment or processes are limited.
It is necessary to verify the supplier’s mold-making equipment, material library, and precision capabilities, to see if they have basic quality systems such as ISO, and to conduct on-site or video inspections of real in-production cases instead of just looking at the quotation sheet.
Neglecting communication and rapid iteration support
The most feared situation in prototype development is when “suppliers only focus on mold making but ignore feedback.”
Excellent suppliers will proactively alert to risks, offer modification suggestions, and support multiple rounds of rapid iterations during the DFM stage.
When conducting an inspection, you might as well directly ask: “Will you proactively conduct a DFM review before mold opening?” How is mold modification charged? Is the feedback timely? The answer is more true than any publicity.
Do not verify the samples and past cases of suppliers
Ask the supplier to provide real samples and cases of similar prototype tooling to see if their surface quality, fit accuracy, and delivery cycle meet the standards.
The results of a one-time mold trial speak louder than verbal promises.
It would be best to visit its workshop or watch the machines online to confirm that the equipment and process capabilities truly exist.
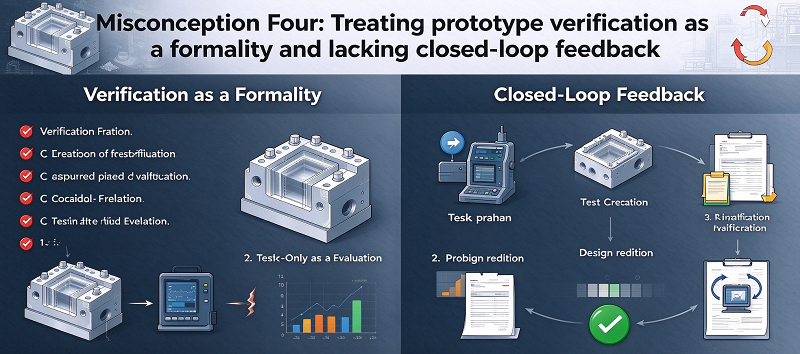
Misconception Four: Treating prototype verification as a formality and lacking closed-loop feedback
The prototype mold is just the beginning. The true value lies in “verifying and driving modifications”.
If one only considers that “the parts can be made” and then ends up hastily, it is equivalent to wasting the most precious error correction window in the prototype stage.
Many projects are repeated precisely because there are no standards for verification and no closed loop for feedback. Once one thing is changed, it triggers another.
Verification should be broken down into three stages: “appearance sample → functional prototype → small-batch trial production”. Clear acceptance standards should be set for each stage. Test results such as dimensions, assembly, life, and failure modes should be fed back into the design to form a closed loop of “design – mold making – verification – modification”.
Each iteration should be based on data rather than intuition.
At the same time, the reasons and results of each modification should be recorded to make the team clear about which designs have been verified to be effective and which are still at risk.
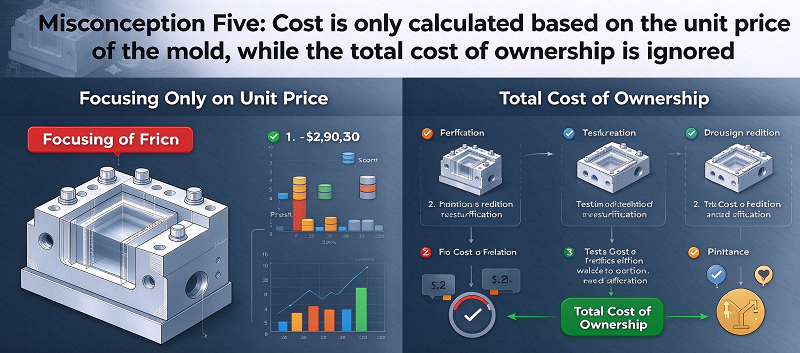
Misconception Five: Cost is only calculated based on the unit price of the mold, while the total cost of ownership is ignored
Only looking at mold quotations is the most common pitfall in prototype cost management.
The true cost = mold fee + unit cost × production quantity + post-processing + rework loss.
Take soft molds, bridge molds, and hard molds as examples: The unit cost of soft molds is medium to low, but their service life is short.
The service life of bridge molds can reach several thousand to tens of thousands of pieces.
Hard molds have the longest lifespan but require a large initial investment.
Selection is essentially a trade-off among cost, quality, and cycle. It is essential to take into account “mold life × unit cost + post-processing” before making a decision, rather than being attracted by a beautiful mold unit price.
After calculating the total cost of ownership, many “cheap” options are actually more expensive. The truly suitable one is often the solution with the best cost performance.
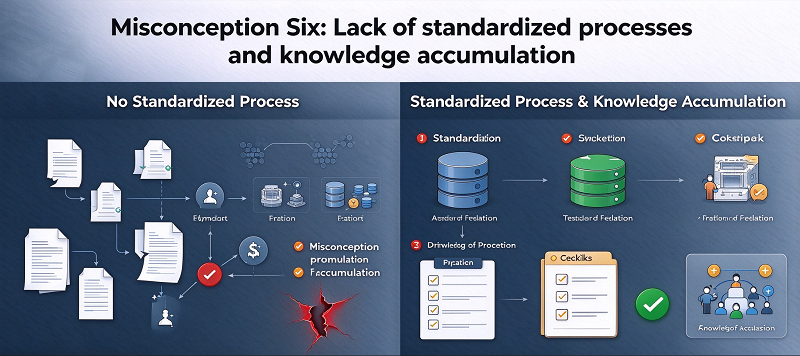
Wanopvatting Ses: Lack of standardized processes and knowledge accumulation
The deep-seated reason why prototype projects keep falling into traps every time they start from scratch and make decisions based on experience.
The lack of processes means that the same mistakes will keep recurring in different projects, and team experience cannot be accumulated as assets.
Accumulate data such as material parameters, tolerance capabilities, and mold life to build the team’s own design specification library.
Establish long-term cooperation with 1-2 reliable suppliers to enable them to better understand your products and avoid the pitfalls they have encountered in the past in advance.
Standardized DFM checklists, acceptance processes, and supplier evaluation forms can make the next prototype project faster and more stable, and also transform experience into the true competitiveness of the team.
7. Hoekom N kiesOBLE as u prototipe tooling mvervaardigingsvennoot
NOBLE is 'n Chinees-Britse gesamentlike onderneming wat deur die regering as 'n "Nasionale Hoëtegnologie-onderneming" toegeken is. Ons het twee hoofbesigheidsrigtings: "Slim Vervaardiging" en "Sorgprodukte". Die "Slim Vervaardiging"-besigheid spesialiseer in die verskaffing van projekondersteuningsdienste aan kliënte, insluitend die bewerking en vervaardiging van onderdele.
Meer as 10 jaar professionele vervaardiging en vinnige prototipering-ervaring. Ons doeltreffende span bied sterk ondersteuning vir u nuwe projekte om 100% aan u vereistes te voldoen; Gestandaardiseerde bestuur bring streng gehaltebeheer van onderdele en produkte; 'n redelike werkvloei behaal laer koste met dieselfde gehalte.
Na jare se harde werk en ontwikkeling het NOBLE geleidelik omskep van 'n presisie-onderdelebewerking- en vervaardigingsonderneming met volledige industriële kettingondersteunende diensvermoëns na 'n diensgerigte onderneming wat volle ondersteuning bied vir kliënte se hele projekte.
NOBLE is your trusted one-stop custom manufacturing solution, from prototype design to manufacturing, with huge manufacturing resources, suitable technology, streamlined processes, expert guidance, and a perfect quality inspection process to turn your ideas into reality.
NOBLE het die volgende kwalifikasiesertifikate:
ISO 9001: 2015 – Robuuste kwaliteitsbestuur vir algemene vervaardiging. Konsekwente prosesse. Gedokumenteerde beheer. Naspeurbare inspeksie.
ISO 13485: 2016 – Strenger kwaliteitsstandaarde vir mediese toestelonderdele. Streng prosesvalidering. Volledige naspeurbaarheid. Vereis vir inplantbare en chirurgiese onderdele.
Gevolgtrekking
Prototype Tooling is not “make the mold first and have a look”, but a decision-making system centered on cost, quality, and cycle.
If you fall into the six major misunderstandings of DFM, material processing, suppliers, verification closed loop, cost accounting, and process accumulation, the cost of rework will increase exponentially.
By conducting pre-DFM, phased closed-loop verification, inferring material processes based on real demands, making decisions based on total cost of ownership, and establishing long-term collaboration and knowledge bases, reliable prototype results can be obtained in the shortest time and at the lowest cost.
Only by treating prototype tools as the “touchstone” of product development rather than a “cost item” can products be pushed to mass production more quickly and steadily in the fierce market competition.
Vrae & Antwoorde
1. What key deliverables should we request from vendors when launching prototype tooling RFQs?
Request a DFM report, sample inspection record, mold lifespan forecast, post-processing quotation, and revised delivery timeline for potential rework.
2. How to define acceptance criteria for prototype parts in formal RFQ documents?
Specify critical fit dimension tolerances, cosmetic surface grade, functional test items, and clear rejection trigger conditions for delivered samples.
3. What risk-related clauses should be included in prototype tooling RFQ terms?
Add clauses for mold repair liability, rework cost allocation, intellectual property protection, and compensation for serious delivery delays.
4. When comparing multiple prototype suppliers via RFQ, what hidden costs should we explicitly ask for?
Ask for charges for DFM review, mold modification, extra sample batches, material switching fees, and surface treatment setup costs.
5. What supporting documentation shall we require suppliers to submit alongside prototype samples per RFQ requirements?
Require material certification, dimensional inspection data, surface-treatment test report, and mold condition summary.





