

The most common ways to make rehabilitation exoskeleton parts are CNC machining, 3D printing, injection molding, sheet metal fabrication, and composite molding. Common materials include aluminum alloys, titanium, stainless steel, PEEK, and silicone for parts that touch the body. These choices affect part strength, weight, biocompatibility, production cost, and lead time. Joint housings need tight tolerances. Custom cuffs need biocompatible surfaces. Frame plates must be strong but lightweight. Each method has clear benefits for certain components. We will look at each process and material in detail. The article also covers design considerations, regulatory standards, and tips for choosing production partners.
Overview of Common Manufacturing Methods for Rehabilitation Exoskeleton Robot Parts
Rehabilitation exoskeleton robot parts fit into a few main groups. Joint assemblies and drive connectors are at the center of every device. Support frames and structural brackets hold everything together. Each group needs strong mechanical properties, because these machines carry human weight and move with the wearer all day.
Key Components of Rehabilitation Exoskeleton Robot Parts
Joint Assemblies and Drive Connectors
Joints are where motion happens. A hip joint, a knee hinge, or a finger pivot must move smoothly and handle repeated load. Drive connectors link motors to these joints, so they must stay lined up under torque. Any looseness in these parts shows up as jerky movement, and that feels wrong to the patient.
Support Frames and Structural Brackets
Frames carry the load path from the body to the ground. Brackets tie actuators, sensors, and straps into one rigid unit. These parts need stiffness, but they also need to stay light. A heavy frame tires the wearer fast.
It is worth noting that process and material choices change by application. An upper limb device has different needs than a lower limb one. Hand exoskeletons often use soft materials, while rigid designs depend on metal. From a practical standpoint, the five process families covered in this article are CNC machining, 3D printing, injection molding, sheet metal fabrication, and composite or silicone molding.
How Process Choice Affects Rehabilitation Exoskeleton Robot Parts
Geometry, Tolerance, and Production Volume
Geometry drives the first decision. Complex contoured shapes push you toward 5-axis CNC or additive methods. Simple flat plates work well with sheet metal. Production volume drives the second. One-off custom cuffs fit 3D printing well, while thousands of identical covers favor injection molding.
Tolerance is the third factor, and it matters most at the joints. The table below shows how CNC and 3D printing compare for joint housings.
| Kriterium | CNC-bearbetning | 3D Utskrifter |
| Precision / Tolerans | Achieves ±0.005 mm on 5-axis titanium joints | Improved for prototyping, not preferred for production-grade end-use parts |
| Ytfinish | Delivers Ra 0.8 or better | Not specified as meeting sterilization-grade finish requirements |
| Materialkompatibilitet | Nearly all medical materials, including Grade 5 titanium and PEEK | Limited compared to CNC for high-strength medical materials |
| Role in Joint Housings | Preferred for critical end-effectors and linkages | Used for prototyping; production parts still rely on CNC |
A ball-and-socket hip joint shows why this matters. The ball must sit in the socket with almost no play. CNC can cut that ball to within a few micrometers, and the socket mirrors it for a snug fit. That level of control is hard to reach with printing alone.
Cost, Speed, and Precision Trade-Offs
Speed and cost pull in opposite directions. CNC gives you precision, but setup takes time. 3D printing skips tooling, so iteration is fast. Injection molding has high upfront tooling cost, yet the unit price drops sharply at volume. Sheet metal bends and punches quickly for flat parts. Pick the process that matches your tolerance target and your batch size, not the one that sounds most advanced.
How Material Choice Affects Rehabilitation Exoskeleton Parts
Strength-to-Weight Ratio and Fatigue Life
Material sets the ceiling on performance. Titanium Grade 5 (Ti-6Al-4V) offers a superior strength-to-weight ratio and is biocompatible, but it is hard to machine and can raise part price by 40-60% versus aluminum. Aluminum 6061-T6 has a 310 MPa yield strength and machines easily at low cost. It suits low-load members and secondary structures.
För konstruktionsramar som inte är implanterade eller steriliserade erbjuder aluminium ett utmärkt förhållande mellan styrka och vikt med lägre material- och bearbetningskostnader. Hårdanodiserad aluminium kan också användas som slitstarka styrningar eller höljen.
Rigid rehabilitation exoskeletons often mix materials. A common setup pairs aluminum frames with stainless steel or titanium joints. This cuts overall weight while adding strength where the load concentrates.
Biocompatibility and Skin Contact
Any surface that touches skin needs care. Silicone works well for cuffs, pads, and liners because it is soft and skin-friendly. Metals used near the body should resist corrosion and clean easily. Material certificates and traceability support this, and they matter for medical exoskeleton robot manufacturing under ISO 13485. The same discipline applies across medical robot parts manufacturing, where every batch must be documented.
Choosing materials and processes together shapes weight, comfort, cost, and safety. Get that pairing right, and the rest of the exoskeleton robot component manufacturing process falls into place.
CNC Precision Machining for Rehabilitation Exoskeleton Parts
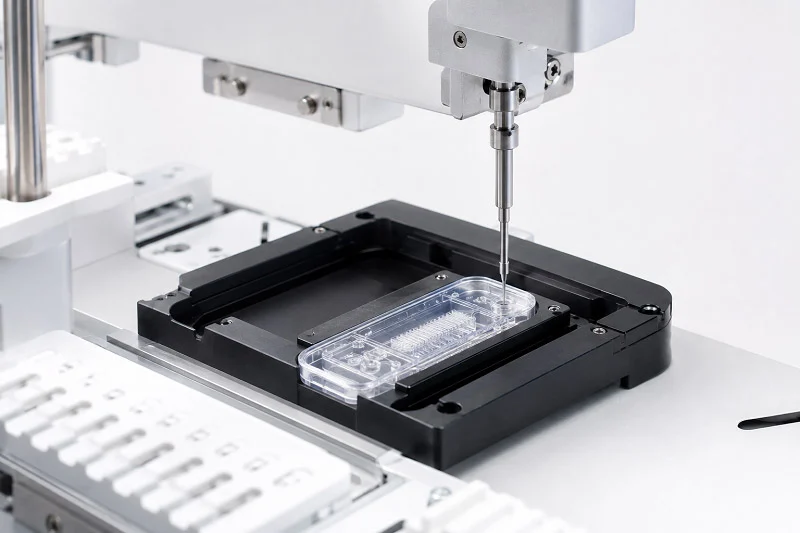
CNC precision machining uses 3-axis, 4-axis, and 5-axis milling machines. Three-axis machines cut simple shapes from one direction. Five-axis machines tilt the tool and the part at the same time. This lets them reach complex curves in one setup. That range matters a lot for rehabilitation exoskeleton robot parts. Joints curve in ways a flat cutter cannot follow.
Applications in Rehabilitation Exoskeleton Parts
Joint Housings and Structural Brackets
Joint housings are very complex and precise parts in exoskeleton systems. They carry the user’s weight and walking impact. They also give exact mounting spots for bearings, reducers, encoders, and torque sensors. The hole for the bearing must stay within 0.1 mm to keep motion accurate. Wall thickness is usually 2–3 mm. Some weight-saving areas are as thin as 1.5 mm. This makes deformation during cutting a real risk. Machining all surfaces in one setup avoids errors from moving the part.
| Applikationsområde | Delexempel | Material | Efterbehandling |
| Gemensamma höljen | Hip joint motor housings, bearing assemblies, positioning shafts, brake interfaces, chain lock blocks | 6061/7075 aluminum alloy (titanium for high-end models) | Sandblasting + anodizing, hard anodizing |
| Motion precision components | Positioning shafts, brakes | 303/304 stainless steel, 42CrMo4 steel | Electropolishing, zinc plating |
| Friction/insulation parts | Connectors and related joint components | POM, nylon, ABS | Used as-is |
Actuator Mounts and Precision Interfaces
Motor and sensor mounting brackets act as precision mounts for electric actuators, torque sensors, and rotary encoders. They often have built-in cable routing channels and mounting bosses. Positioning shafts and robot joint housings usually need concentricity within ±0.01 mm. This keeps bearings seated smoothly and prevents wear. A custom machined exoskeleton stator mount follows the same logic. Use 3-axis machining for flat brackets with simple holes. Switch to 5-axis when the mount wraps around an actuator or has angled faces.
Advantages for Rehabilitation Exoskeleton Parts
Snäva toleranser och repeterbarhet
CNC holds tolerances that printing and molding cannot match on metal. Every cycle repeats the same tool path. So part one and part one thousand line up. The FreeGait active exoskeleton adjusts thigh and shin length and hip width for different body types. The precision of each connector directly affects wearing comfort. Repeatability is what makes that adjustment reliable.
Ytbehandling och efterbearbetning
Machined surfaces come off the tool smooth. Secondary steps push them further. Anodizing, polishing, and coating add corrosion resistance. Sandblasting plus anodizing is common on aluminum housings. Electropolishing works well for stainless steel. These finishes also make cleaning easier. That matters for parts near skin.
Typical CNC Materials for Rehabilitation Exoskeleton Parts
Aluminiumlegeringar (6061, 7075)
Aluminum alloy gives an ideal strength-to-weight ratio for dynamic motion and extended use. It machines fast and keeps costs down. Custom machined exoskeletons often use aluminum alloy frames and mounts as basic structures. Hip, knee, and shoulder joint assemblies all rely on it.
Titanium (Grade 5 Ti-6Al-4V) and Stainless Steel (316L)
Titanium is biocompatible, lightweight, and corrosion-resistant. It works well for high-end models. Stainless steel resists wear and handles sterilization. Both materials cost more and cut slower than aluminum. So save them for loaded joints and precision mechanical parts. The RoboGait system got about 90% of its mechanical parts from outside suppliers. This covered CNC milling, turning, laser cutting, bending, and welding. It shows that CNC-machined parts anchor real rehabilitation exoskeleton parts programs.
3D Printing for Rehabilitation Exoskeleton Parts
3D printers can make many different exoskeleton robot parts. This includes connectors, brace supports, and battery pack internals. The technology works best when shapes are complex or when you only need a few units. For rehabilitation exoskeleton robot parts, printing gives speed and design freedom that old methods cannot easily match.
Applications in Rehabilitation Exoskeleton Parts
Custom-Fit Cuffs and Limb Interfaces
Every patient has a different body shape. A cuff that fits one person well may cause pressure sores on another. 3D printing fixes this by building cuffs straight from scan data. You scan the patient’s limb shape, design the interface in CAD, and print it as one piece. The result is a custom exoskeleton parts solution that feels comfortable right away.
Prototypframställning och lågvolymproduktion
Prototyping is where printing really shines. You can test a new joint design, change the wall thickness, and reprint overnight. There are no tooling costs and no minimum order amounts. For low-volume production runs, printing stays cost-effective when you need fewer than a few hundred units. It also supports indirect digital manufacturing. You can print reusable molds for soft hand exoskeleton actuators, then cast silicone parts from those molds.
Advantages for Rehabilitation Exoskeleton Parts
Design Freedom and Lattice Structures
Printing removes many design limits. Internal channels, organic shapes, and lattice structures all become possible. Lattice infill cuts weight while keeping strength. That matters for wearable devices, where every gram counts.
Rapid Iteration and Patient-Specific Geometry
Design changes happen fast with printing. You change the CAD file and print again. There is no waiting for new tooling. This speed supports patient-specific geometry, which is key for pediatric devices and custom orthoses.
Typical 3D Printing Materials
Nylon PA12 and PA11 for SLS and MJF
Nylon PA12 is a standard material for SLS and MJF processes. It offers even mechanical properties, chemical resistance, and living-hinge capability. PA11 is similar but made from plants. Both work well for cuffs, housings, and non-structural brackets.
Titanium and Stainless Steel for DMLS and SLM
Metal printing uses DMLS or SLM processes. Titanium Ti-6Al-4V (Grade 5) is body-safe and resists corrosion. Stainless steel 316L also prints well and handles sterilization. These materials suit load-bearing implants and high-stress joints. The table below compares key properties.
| Fast egendom | Nylon PA12 | Titan Ti-6Al-4V (Grad 5) |
| Materialkategori | Nylon | Metall |
| Brottgräns | 48 MPa | 950 MPa |
| Densitet | 1.01 g / cm3 | 4.43 g / cm3 |
| Glasövergångstemperatur | 175 ° C | 1650 ° C |
| Förlängning | 20.0% | 14.0% |
| Common 3D printing processes | SLS, MJF | CNC-3, CNC-5, DMLS |
The choice between nylon and metal depends on load requirements. Nylon suits body-contact parts and light structural pieces. Titanium and stainless steel handle high loads and repeated stress cycles. Both material families support the manufacturing of rehabilitation exoskeleton parts across different device types.
Injection Molding for Rehabilitation Exoskeleton Parts
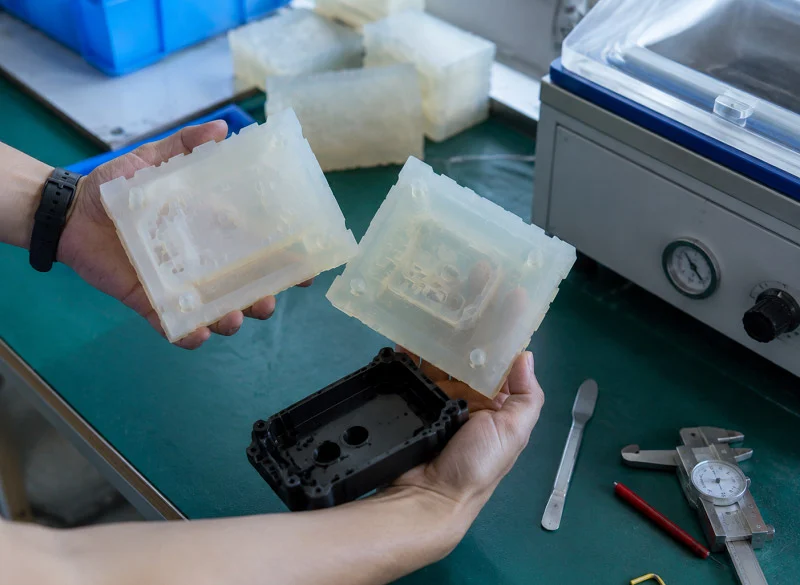
Injection molding works best when you need thousands of identical plastic pieces. The process pushes melted plastic into a steel mold. Then the mold cools, opens, and drops out a finished part. For rehabilitation exoskeleton robot parts, this method makes covers, housings, and cable clips in large amounts.
Applications in Rehabilitation Exoskeleton Parts
Covers, Housings, and Cable Management
Every exoskeleton needs protective shells. Motor covers keep dust out. Control box housings protect circuit boards. Cable management clips route wires along the frame. These parts share one thing in common. They have complex shapes but do not carry heavy loads. Injection molding handles that mix well. You get smooth surfaces, built-in snap fits, and even wall thickness in one cycle.
High-Volume Connectors and Fasteners
Small connectors and fasteners add up quickly. A single exoskeleton might use dozens of clips, plugs, and mounting tabs. Molding these parts keeps unit costs low once production speeds up. The process also holds tight dimensions. That matters when a connector must snap into place thousands of times.
Advantages for Rehabilitation Exoskeleton Parts
Low Unit Cost at Scale
Tooling for injection molding costs money upfront. Steel molds can cost thousands of dollars. But that cost spreads across every part you make. At low volumes, CNC and 3D printing win. At high volumes, molding becomes the clear choice. The break-even point depends on part size and mold complexity. For small covers and clips, molding often beats CNC once you pass a few thousand units.
Consistent Material Properties and Color Options
Molded parts come out identical. The same resin, the same temperature, the same pressure every cycle. You get predictable strength and fit. Color matching is easy too. Just add pigment to the resin. No painting or coating needed. That saves time and avoids chipping.
Typical Injection Molding Materials
PEEK and PEI for High-Strength Applications
Medical-grade PEEK handles high temperatures and repeated sterilization. It also resists chemicals and wear. PEI offers similar benefits at a lower cost. Both materials suit structural covers and load-bearing housings. They cost more than common plastics, but they last longer in demanding environments.
ABS, PC, and TPU for Flexible or Impact-Resistant Parts
ABS is tough and easy to mold. PC adds impact strength and clarity. TPU brings flexibility for grips and soft touch points. These materials cover most non-critical exoskeleton robot parts. The table below compares their key traits.
| Material | Nyckelegendom | Allmänt bruk |
| ABS | Tough, easy to mold | Covers, housings |
| PC | Hög slaghållfasthet | Protective shells |
| TPU | Flexibel, mjuk | Grips, pads |
Choosing the right resin depends on load, sterilization needs, and cost targets. For many rehabilitation exoskeleton parts, standard plastics do the job well.
Sheet Metal Fabrication for Rehabilitation Exoskeleton Parts
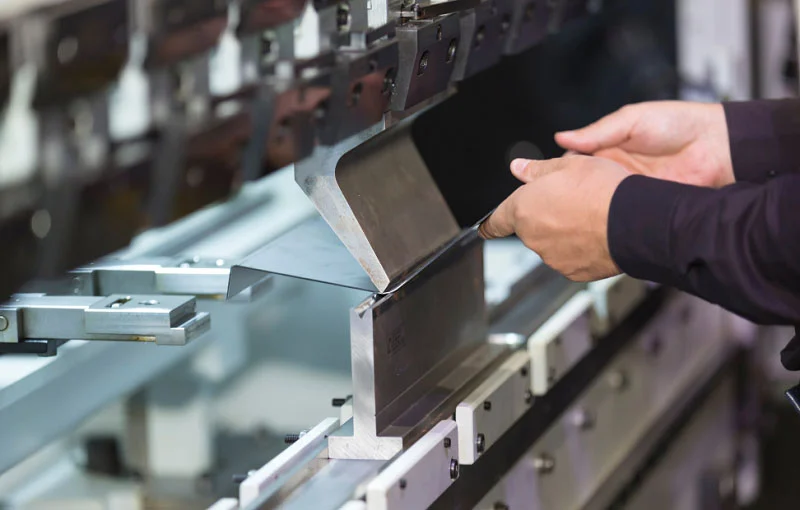
Sheet metal fabrication takes flat sheets and turns them into strong, lightweight parts. First, it cuts the metal. Then it bends and punches it. CAM sheet metal bending is a key step in this process. It shapes complex parts like an exoskeleton hand with exact angles and curves. For rehabilitation exoskeleton robot parts, this method makes frame plates, sensor brackets, and mounting plates at a low price.
Applications in Rehabilitation Exoskeleton Parts
Frame Plates and Structural Supports
Frame plates are the backbone of many exoskeleton designs. They connect joints, hold loads, and keep everything lined up. A typical frame plate might be several millimeters thick. It gets bent into a channel or L-shape to become stiffer. These parts often carry the main load in lower-limb devices.
Sensor Brackets and Mounting Plates
Sensors need stable spots to mount. A small shift can mess up angle readings or force measurements. Sheet metal brackets hold encoders, IMUs, and force sensors in place. Mounting plates also hold control boxes and battery packs. These exoskeleton robot parts are simple in shape but very important for system accuracy.
Advantages for Rehabilitation Exoskeleton Parts
Cost-Effective for Thin, Flat Shapes
Sheet metal works best when parts are thin and flat. Cutting and bending cost much less than CNC milling a solid block. You also waste less material. For large frame plates, this price gap grows fast. A stamped or laser-cut plate might cost a fraction of a machined one.
Fast Turnaround for Prototypes and Small Batches
Prototyping goes fast with sheet metal. You can laser-cut a design in hours, bend it, and test the fit the same day. No tooling is needed for small batches. This speed helps teams improve frame geometry without waiting weeks for molds or castings.
Typical Sheet Metal Materials
Aluminum and Stainless Steel Sheets
Aluminum alloy sheets like 5052 or 6061 give a great strength-to-weight ratio. They resist rust and bend easily. Stainless steel sheets add more strength and better wear resistance. Grade 304 and 316 are common choices. Stainless steel costs more, but it stands up to harsh cleaning and sterilization. The table below compares key traits.
| Material | Nyckelegendom | Allmänt bruk |
| aluminiumlegering | Light, resists rust | Frame plates, brackets |
| Syrafast | Stark, motstår slitage | Sensor mounts, load plates |
Surface Treatments for Wear and Rust Resistance
Aluminum parts often get anodized for protection. Two methods stand out for exoskeleton frame plates:
- Micro-Arc Oxidation (MAO) and hard anodizing create a dense, bonded ceramic coating over complex shapes.
- Sealed hard-anodized or MAO-coated surfaces can handle extended salt spray testing without pitting. They also fully seal the surface to stop stress corrosion cracking in damp or outdoor settings.
These treatments make parts last longer and keep the device safe for daily use. Picking the right materials and finishes for rehabilitation exoskeleton parts pays off in durability and comfort for the user.
Composite and Silicone Molding for Rehabilitation Exoskeleton Parts
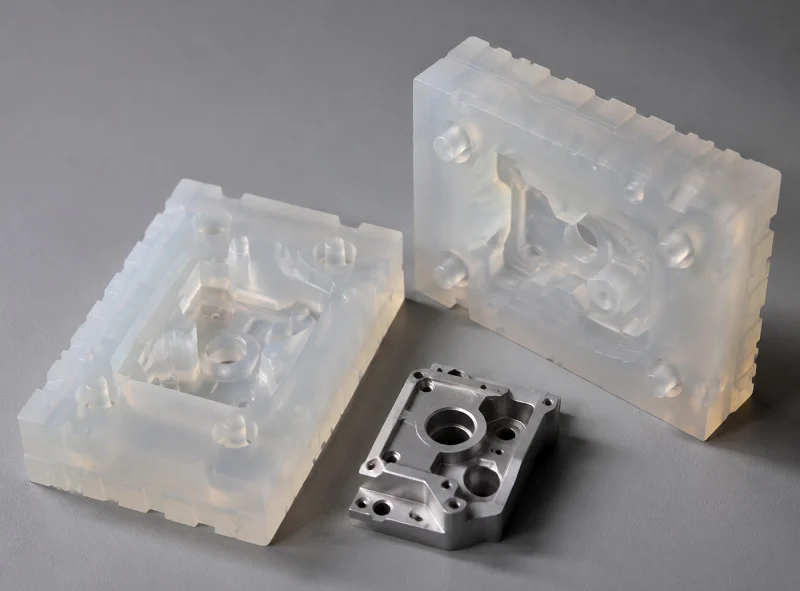
Composite parts are strong but weigh very little. Carbon fiber and fiberglass layups give stiffness that metal cannot match at the same weight. Silicone parts stay soft where the device touches skin. These two material families do different jobs. Both are needed in modern exoskeleton robot parts.
Composite Processes for Rehabilitation Exoskeleton Parts
Layup Techniques and Compression Molding
Layup begins with sheets of fiber fabric. You put them into a mold one layer at a time. Epoxy resin holds the fibers together. For compression molding, you place the fiber between two mold halves. A hydraulic molding table uses high pressure and heat. This shapes and hardens the part in one step. The process is efficient, accurate in size, and low in cost. It makes high-quality finished parts with steady properties. Frame plates and structural shells work well with this method. It suits parts that need strength in one main direction.
Resin Transfer Molding for High-Strength Components
Resin Transfer Molding (RTM) uses a different setup. It depends on a rigid two-part mold. The mold holds reinforcement fiber or a preform inside. The resin-catalyst mixture melts in a heated transfer pot. A piston pushes it into the mold cavity under pressure. Low pressure and low temperature keep the process steady throughout. The mold stays closed until the resin fully hardens. After curing, you take out the finished component. Variants like vacuum infusion and vacuum-assisted RTM also exist. Key settings such as heating time, melting temperature, applied force, and cooling time need careful control. RTM suits complex shapes that need even wall thickness and few voids.
Silicone Molding for Rehabilitation Exoskeleton Parts
Body-Contact Cuffs, Pads, and Liners
Parts that touch the user’s body are often made from silicone. This material is light and gentle on skin. Cuffs wrap around the thigh or arm. Pads cushion pressure points. Liners sit between the rigid frame and the wearer’s skin. Liquid silicone rubber injection molding is the standard process for these parts. The material flows into a heated mold and cures into a flexible solid. A well-made silicone part has no seams or sharp edges. That matters for comfort over long periods.
Lightweight and Skin-Friendly Properties
Silicone has low density. It helps keep the whole device lighter. It does not irritate skin or cause allergic reactions. The surface stays grippy but soft enough to prevent pressure sores. Cleaning is easy with soap and water or medical disinfectants. These traits make silicone a top choice for any surface that touches the wearer directly. It is worth noting that silicone also fights bacteria growth.
When to Choose Composites or Silicone
Weight Reduction vs. Structural Rigidity
Composites win when you need stiffness with low weight. A carbon fiber frame plate weighs much less than an aluminum one at the same thickness. But composites cost more to make. The molding process needs tooling and skilled workers. Silicone wins when flexibility matters more than rigidity. Choose composites for load-bearing structures. Choose silicone for comfort interfaces.
Comfort, Hygiene, and Durability
Silicone parts resist sweat, oils, and bacteria. They can be wiped clean or sterilized. Composite parts are harder to clean because the surface is more porous. For long-term wear, silicone stays comfortable and hygienic. Composites keep their structure strong over many cycles. Both materials matter in making modern rehabilitation exoskeleton parts. From a practical view, the smart approach is to use each where it works best.
Material Properties Critical for Rehabilitation Exoskeleton Parts
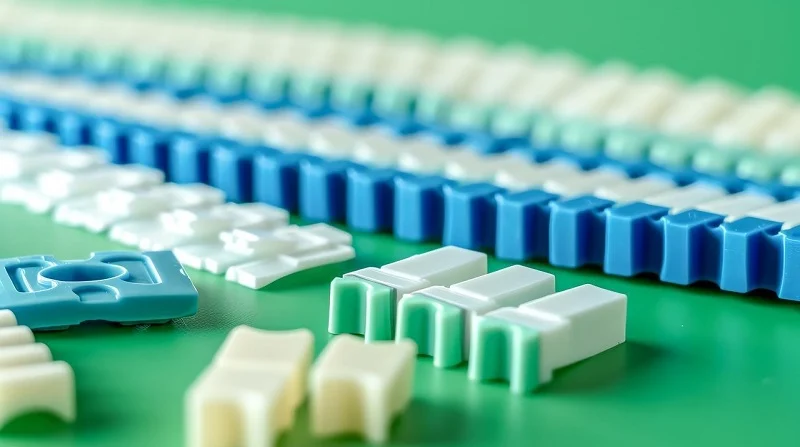
Picking the right material for rehabilitation exoskeleton parts is not just about strength. It is about safety, comfort, and how long the device lasts. A frame that feels too heavy will tire the patient. A cuff that irritates skin will get taken off. So the material properties you choose affect how the user feels.
Biocompatibility and Skin Safety in Rehabilitation Exoskeleton Parts
ISO 10993 and Cytotoxicity Requirements
Any material that touches skin must pass strict safety tests. ISO 10993-5:2009, Part 5, gives the rules for in vitro cytotoxicity testing. This test checks if a material kills cells. In one study on a skin-contact material, extracts were made by soaking the material in serum-free medium at various concentrations for 72 hours. The extracts were then filtered before being added to cell cultures. The concentration range was chosen to avoid problems from thickness that could affect cell shape, movement, and function. This kind of testing proves a material will not harm the wearer.
Appropriate analysis and non-clinical testing (such as that outlined in the currently FDA-recognized editions of ANSI/AAMI/ISO 10993-1, “Biological Evaluation of Medical Devices—Part 1: Evaluation and Testing Within a Risk Management Process,” ANSI/AAMI/ISO 10993-5, “Biological Evaluation of Medical Devices—Part 5: Tests for In Vitro Cytotoxicity,” and ANSI/AAMI/ISO 10993-10, “Biological Evaluation of Medical Devices—Part 10: Tests for Irritation and Skin Sensitization”) must validate that the skin-contacting components of the device are biocompatible.
Hypoallergenic and Non-Toxic Material Options
Some people react badly to certain metals. Nickel is a common cause. That is why medical-grade stainless steel 316L and titanium are safer choices for body-contact parts. Silicone also works well because it does not cause allergic reactions. It stays soft and grippy. For any surface that touches skin, check the material certificate. It should confirm the alloy or polymer meets biocompatibility standards.
Strength and Fatigue Resistance in Rehabilitation Exoskeleton Parts
Yield Strength and Load-Bearing Capacity
Yield strength tells you how much load a part can take before it bends for good. Aluminum alloy 6061-T6 has a yield strength of 310 MPa. That handles low-load parts and secondary structures well. Titanium Grade 5 pushes much higher. It fits joints and brackets that carry the user’s full weight. Stainless steel 316L sits in between. It resists wear and handles sterilization. The load path through the device decides which material goes where.
Cyclic Loading and Long-Term Durability
Exoskeletons move with the wearer. Every step, every reach, every grip adds a load cycle. Over thousands of cycles, small stresses can crack a part. This is called fatigue. Materials with high fatigue resistance last longer. Titanium and stainless steel work well under repeated stress. Polymers like PEEK also hold up, but they have limits. Designers should test prototypes under real-world cycles. A part that survives the lab might fail in daily use.
Weight and Comfort in Rehabilitation Exoskeleton Parts
Density Comparisons Across Metals and Polymers
Weight matters a lot for wearable devices. A heavy frame tires the patient fast. Density is the key number here. Lower density means less weight for the same volume. The table below compares common materials.
| Material | Yield Strength (MPa) | Trötthetsresistens |
| Aluminium 6061-T6 | 310 | Moderate |
| Titan Ti-6Al-4V | Hög | Hög |
| Rostfritt stål 316L | Moderate | Hög |
| TITT | Moderate | Moderate |
| Nylon PA12 | 48 | Låg |
| Silikon | ej tillämplig | Låg |
Aluminum alloy offers a high strength-to-weight ratio at low cost. Titanium costs more but saves weight while adding strength. PEEK and nylon are much lighter than metals. They work well for covers and non-structural parts. Silicone stays soft and light for cuffs and pads.
Balancing Stiffness with Wearer Comfort
Stiffness keeps the device lined up. Too much stiffness feels rigid and uncomfortable. Too little stiffness lets parts flex and go out of line. The goal is a balance. Use rigid materials at the joints and frame. Use soft materials at contact points. This mix keeps the device stable without losing comfort. Material selection here is not about one perfect choice. It is about pairing the right properties for each part. From a practical view, that pairing is what makes a rehabilitation exoskeleton feel like a tool instead of a burden.
Case Studies of Exoskeleton Robot Parts
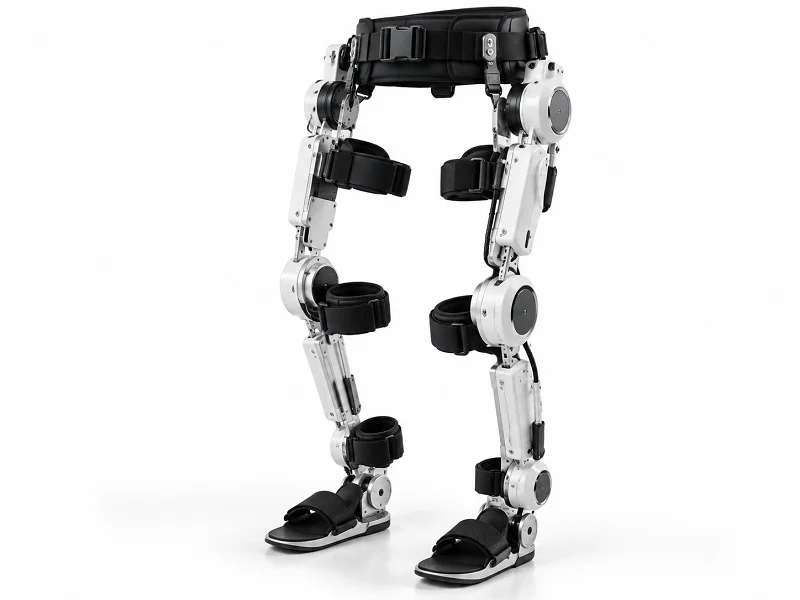
Joint Housing for a Lower-Limb Rehabilitation Exoskeleton Part
Process and Material Selection Rationale
A lower-limb device needs a hip joint housing that holds the wearer’s full weight while walking. The design team chose 7075 aluminum alloy for this part. This material has a great strength-to-weight ratio and is fast to machine. The housing has bearing bores that must stay within 0.1 mm to keep motion smooth. Five-axis CNC machining was the clear choice here. It cuts all surfaces in one setup, so the part stays accurate. Hip joint motor housings often use this same approach.
Performance and Production Outcomes
The finished housing passed fatigue testing under thousands of load cycles. Part weight dropped compared to an earlier steel version. Production runs stayed repeatable, with every unit matching the first. This case shows how material selection and process choice work together for rehabilitation exoskeleton parts.
Sensor Mount for an Upper-Limb Rehabilitation Exoskeleton Part
Design Constraints and Manufacturing Method
An upper-limb device needed a bracket to hold a torque sensor near the elbow. The mount had to fit inside a tight space and keep the sensor aligned within ±0.01 mm. It also needed built-in cable routing. Three-axis CNC was enough here because the part had flat faces and simple holes. No complex curves meant no need for five-axis work.
Material Choice and Integration Challenges
The team chose 316L stainless steel for its wear resistance and easy cleaning. This material handles sterilization well. The main challenge was integrating the sensor without adding bulk. The final design used a thin plate with mounting bosses. It fit perfectly and kept readings stable.
Custom Cuff for a Pediatric Rehabilitation Exoskeleton Part
Patient-Specific Requirements and 3D Printing
Children grow fast, so a standard cuff rarely fits for long. The team used 3D printing to build cuffs straight from scan data. Nylon PA12 worked well for this application. It is light, tough, and flexible enough for comfort. Each cuff matched the child’s limb shape exactly.
Biocompatibility and Comfort Validation
The cuff passed ISO 10993 cytotoxicity testing. Silicone padding added softness at pressure points. Parents reported no skin irritation after weeks of use. This case proves that manufacturing can adapt to each patient when the process fits the need.
Regulatory and Quality Standards for Rehabilitation Exoskeleton Parts
Rules shape how you build rehabilitation exoskeleton parts. They also decide which markets you can sell into. Two big frameworks matter most. One comes from the FDA. The other comes from the European Union.
Medical Device Standards for Rehabilitation Exoskeleton Parts
ISO 13485 and Quality Management Systems
ISO 13485 sets the quality management rules for medical devices. It covers design, production, and steps taken after the product is sold. EU MDR points to this standard through its conformity assessment annexes. But having ISO 13485 certification by itself does not meet MDR. You still need documents that are specific to your product.
FDA Quality System Regulation and EU MDR Requirements
The FDA calls its Quality System Regulation. Recent updates brought it closer in line with ISO 13485. This turns into the Quality Management System Regulation (QMSR). The table below shows how the two frameworks are different.
| Dimensionera | FDA:s kvalitetssäkringsrapport | EU MDR |
| Regulatory philosophy | Quality system focused on manufacturing processes | Full product regulation across the device lifecycle |
| Quality system alignment | Aligned with ISO 13485, plus FDA-specific rules | References ISO 13485, but needs more product documents |
| Kliniska bevis | Varies by pathway (PMA vs. 510(k)) | Requires structured clinical evaluation |
| UDI system | FDA UDI with its own database | UDI in EUDAMED, separate from FDA |
| Övervakning efter marknaden | Less prescriptive | Explicit PSURs, PMCF, and ongoing surveillance |
| Authorization route | 510(k) Clearance or PMA Approval | Notified Body review and CE Marking |
MDR Class III devices are about the same as FDA Class III devices or new Class II devices that need a PMA. MDR Class IIa and IIb devices match up with moderate-risk FDA Class II devices that get cleared through 510(k).
Material and Process Certifications for Rehabilitation Exoskeleton Parts
ISO 9001 and Consistent Production
ISO 9001 helps molded and machined parts come out the same every time. Before sampling, a pre-production mold inspection checks that the tooling is accurate. In-process monitoring keeps temperature, pressure, and cycle times within set limits. Final inspection confirms the dimensions and how the part looks. Material certifications and inspection records support traceability. This discipline raises the quality of medical robot parts in every run.
Based on ISO 9001 and IATF 16949 certifications, robotics products are rigorously tested, with quality checks built into the production process to ensure finished assemblies withstand physical demands and meet stringent specifications.
Biocompatibility and Sterilization Standards
Parts that touch skin must pass ISO 10993 testing. Cytotoxicity, irritation, and sensitization tests prove they are safe. Sterilization methods are different for each material. Some plastics can handle autoclave heat. Others need ethylene oxide or gamma radiation. The material you pick and the sterilization method must go together. This biocompatibility and sterilization tolerance keeps patients safe.
Documentation and Traceability for Rehabilitation Exoskeleton Parts
Device Master Records and Batch Records
Every rehabilitation exoskeleton part needs a device master record. It holds design specs, drawings, and process steps. Batch records track what happened during manufacturing. These files prove each unit meets its spec.
Material Certificates and Process Validation
Material certificates confirm the alloy or polymer grade. Process validation shows the method works every time. Precision inspection closes the loop. It catches drift before bad parts ship. From a practical perspective, strong documentation protects both the patient and the manufacturer.
NOBLE: Manufacturing Rehabilitation Exoskeleton Parts from Design to Assembly

NOBLE works with metal and plastic parts for exoskeleton components. The company runs all the methods we talked about in this article. CNC machining, 3D printing, injection molding, and sheet metal all happen under one roof. Most exoskeletons mix materials. Strong metals go into joints and frames. Plastics and silicone cover the rest. Having one partner cuts down on handoffs between different suppliers.
Expertis inom metall- och plastbearbetning
CNC Machining, 3D Printing, Injection Molding, and Sheet Metal
NOBLE runs all four types of processes. CNC machines cut joint housings with very tight tolerances. Five-axis setups handle complex curves on hip and knee parts. The CNC department works around the clock for repeat orders. 3D printers build custom cuffs from patient scan data. Injection molding makes covers in large amounts. Sheet metal fabrication bends frame plates in hours for prototypes.
Materialval och processoptimering
The right material depends on what the part does. Load-bearing joints need strong metals like titanium or aluminum. Cuffs need soft silicone or nylon. Plastic covers work well with ABS or PC. No single material works for everything. NOBLE’s team helps pick the best combination. They match the right material to the right process for each part. This pairing keeps quality up and production costs down. A part that needs tight bores goes to a CNC center for precision work.
Certifieringar och kvalitetssäkring
ISO 9001 och ISO 13485
Norman Noble holds ISO 13485 certification, maintaining the standard over many years.
NOBLE also follows ISO 9001. This standard makes sure parts stay the same across every run. Every process follows written steps. Every shift uses the same settings. Together with the ISO 13485 certification, these standards give customers confidence in each batch they get.
Full Traceability and Inspection
Every batch gets recorded from start to finish. Material certificates confirm the alloy or polymer grade. Inspection records track dimensions and surface finish. If any size goes out of spec, the records show when and why. This level of detail helps with audits without extra work.
End-to-End Services for Rehabilitation Exoskeleton Parts
Design, Prototyping, Production, and Assembly
NOBLE handles the whole chain for rehabilitation exoskeleton parts. Design teams make parts easier to build with the chosen process. Prototyping tests fit before production starts. Production scales to whatever volume you need. Assembly puts everything together into finished devices.
Partnering from Concept to Finished Device
Getting involved early makes a big difference in exoskeleton design and manufacturing. NOBLE’s team advises on material choices, process selection, and design for manufacturing. This shortens lead times and cuts rework. The result is a smoother path from concept to finished device.
The five process families covered—CNC precision machining, 3D printing, injection molding, sheet metal fabrication, and composite or silicone molding—each work best for different rehabilitation exoskeleton parts. Aluminum alloy is good for frames when weight matters. Stainless steel handles high-load joints and resists rust well. It is a strong choice near the body. Aluminum alloy fits secondary parts where saving weight counts. Pick your process by needed accuracy and how many parts you make. CNC gives tight tolerances and repeatable results for complex parts. A good manufacturing partner has ISO 13485 certification and handles everything from design to assembly. Quality manufacturing keeps every batch traceable. In the future, new methods will make exoskeleton parts lighter, safer, and more custom-fit for each patient.
FAQ of Rehabilitation Exoskeleton Parts
What manufacturing method should I pick for rehabilitation exoskeleton parts?
It depends on the part’s shape, how exact it needs to be, and how many you need. CNC works well for metal joints that need tight tolerances. 3D printing is good for custom cuffs and early models. Injection molding is best for making many plastic covers at once. Sheet metal works for flat frame plates. Pick the method that fits what you need.
Which materials are safe for skin-contact exoskeleton parts?
Silicone is the best choice for cuffs and pads. It stays soft, fights bacteria, and passes ISO 10993 tests. Medical-grade stainless steel 316L and titanium are also safe near skin. Stay away from materials that have nickel.
How do CNC machining and 3D printing compare for exoskeleton joints?
CNC can hit ±0.005 mm tolerances on titanium or aluminum joints. It is the top pick for production parts that are ready to use. 3D printing is best for early models and custom-fit cuffs, not for load-bearing joints that need tight tolerances.
What regulatory standards apply to rehabilitation exoskeleton parts?
ISO 13485 covers quality management. FDA quality system regulations or EU MDR rules apply based on where you sell. Parts that touch skin must pass ISO 10993 biocompatibility tests.
Can you use different materials in one exoskeleton device?
Yes. A common mix pairs aluminum frames with titanium or stainless steel joints. This saves weight where the load is low and adds strength where stress builds up.
When does injection molding make sense for exoskeleton parts?
Injection molding saves money once you need thousands of identical plastic parts. It works well for covers, housings, cable clips, and connectors.
What surface treatments help exoskeleton parts last longer?
Aluminum parts get hard anodizing or micro-arc oxidation. Stainless steel gets electropolishing. These coatings fight wear, rust, and cleaning chemicals.
Is nylon or silicone better for custom exoskeleton cuffs?
Silicone is softer and gentler on skin for body-contact cuffs. Nylon PA12 is tougher and works for structural parts that need some flex. Choose silicone for comfort, nylon for strength.






